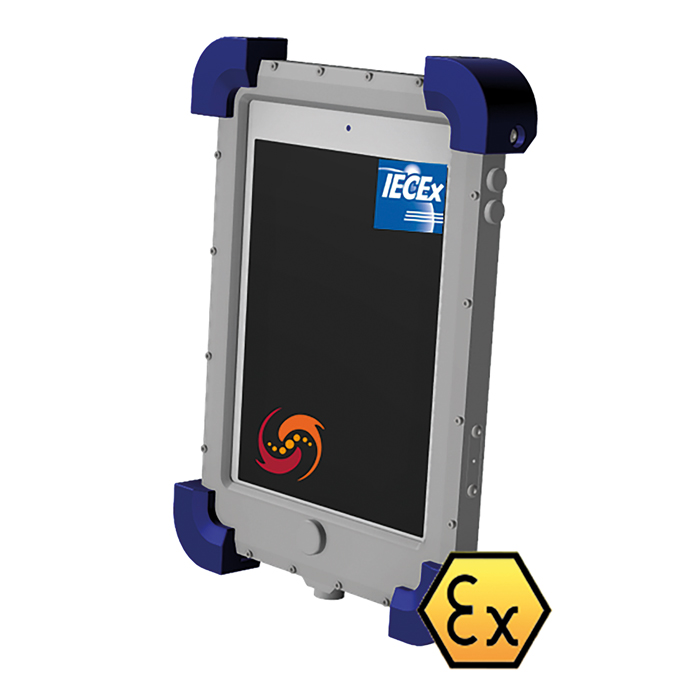
ECOM Presents World’s First 10” Android Tablet for Hazardous Areas

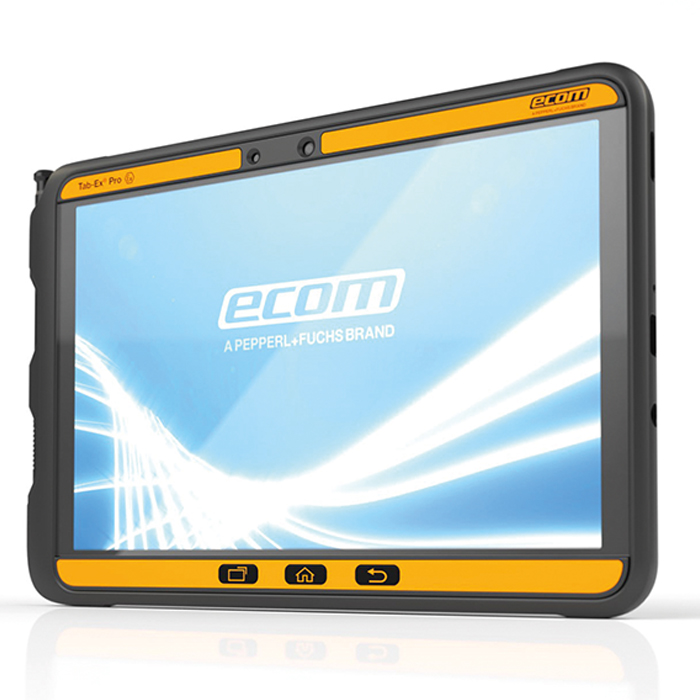
The Tab-Ex® Pro from the Pepperl+Fuchs brand ECOM expands the Tab-Ex series as the world’s first 10-inch Android tablet for Zone 2/22 and Div. 2 hazardous areas. The Tab-Ex® Pro’s large display is ideal for demanding applications and for accessing web-based content. In addition, it allows employees to easily transition from working in the field to working at the office. 

Flexibility for Mobile Workers

ECOM developed the Tab-Ex® Pro to keep up with Industry 4.0 and the associated demands on mobile devices. The new tablet enables customers to meet the challenges of digitalization while simplifying the way employees work in increasingly complex environments.

The tablet’s 10-inch screen is perfectly suited for displaying and interacting with interactive, web-based, and augmented reality content and apps, even in hazardous areas. This is helpful, for example, when the device is used to call up a construction drawing or to receive instructions for certain work steps. The tablet is lightweight and easy to use despite its large screen and rugged construction.

Added Safety with New Technology and Industry Standards

The Tab-Ex® Pro is based on Samsung’s Galaxy Tab Active Pro tablet, with features such as Google AR Core, facial recognition, and a Qualcomm SDM670 Octa-Core 64 bit 2.0 GHz, 1.7 GHz processor. Samsung KNOX and Android 9 (Android 10 is planned) guarantee high data and device security. With the help of Samsung DeX mode, users can connect the tablet to a large screen and keyboard for a complete desktop experience.

Pogo pin charging and a powerful replaceable battery with a capacity of 7,400 mAh ensure smooth operation and 15 hours of runtime in the field. Peripherals such as headsets, remote speaker microphones, and a smartwatch enhance the practicality and functionality of the Tab-Ex® Pro. The tablet is also available without a camera upon request.

Additionally, the Tab-Ex® Pro supports applications for lone worker protection, which are especially necessary for industrial use and in hazardous areas. Like all ECOM devices, the Tab-Ex® Pro is equipped with a programmable button for fast and effective emergency calling. The microphone and loudspeaker connections designed for Zone 2/22 and Div. 2 always ensure effective communication.

Designed for Industry 4.0

The Tab-Ex® Pro is perfectly tailored to applications in the oil and gas, chemical, pharmaceutical, food and beverage, and aviation industries. Fast data access and management enhances worker efficiency and productivity, and the possibility of direct communication with colleagues and experts at other locations means that maintenance and servicing can be carried out more effectively. The tablet can also be operated with gloves.

With ARCore, the Tab-Ex® Pro is designed for augmented reality applications and other Industry 4.0 tasks. This makes the device a useful tool today and for the applications of the future. The device also supports the lone worker concept, which means it can protect employees distributed across a wide geographical area. 

Whether plant management, inventory management, process automation, maintenance, or applications in transport and logistics, the Tab-Ex® Pro simplifies processes and minimizes risk in industrial environments. The new product will be available with NEC/CEC approval starting in September and with ATEX/IECEx approval starting in October.
www.ecom-ex.com

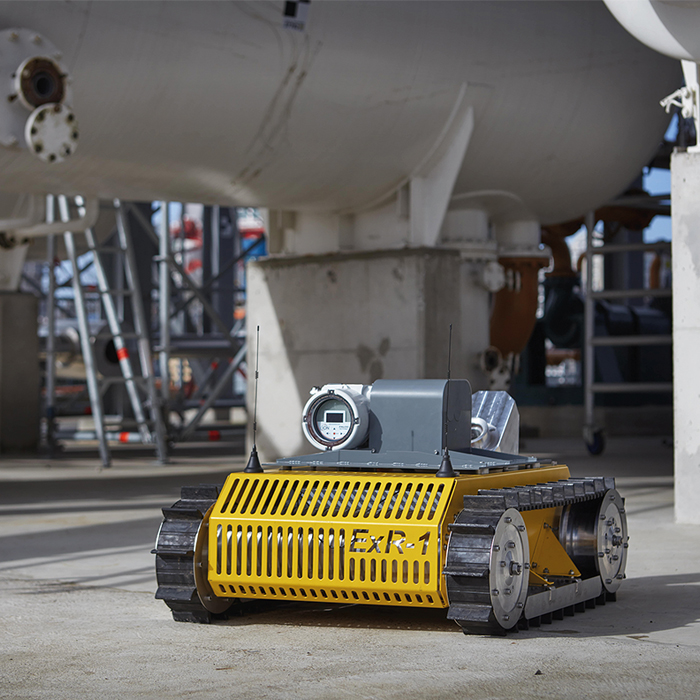
Exrobotics’ EXR-1 Unmanned Facilities Surveillance Robot Incorporates Falco For Autonomous Gas Detection 

ATEX & IECEx Zone 1 accredited robot incorporated with the ION Science Falco for the detection of VOCs in flammable and explosive environments

Throughout unmanned facilities within the oil and gas industry, a human presence is generally still needed for regular inspection work, so deploying Ex certified robots (ATEX and IECEx Zone 1) incorporated with the ION Science Falco, can have a significant positive impact on safety by minimising worker field trips, which in turn reduces operating costs.

Explosion proof ATEX Zone 1 iPad for ATEX and IECEx

Atexxo Manufacturing has released an Apple iPad mini 5 which is suitable for use in Zone 1 and Zone 2 hazardous locations. The explosion proof iPads are originally manufactured by Apple then converted and certified according to ATEX and IECEx by Atexxo Manufacturing.

This makes the ATEX and IECEx tablets suited for safe use in gas/vapour Zone 1 and zone 2 hazardous areas. Sim-card can be installed by the end-user themselves, or eSim can be used. The devices are suited for Apple (open) DEP enrollment program.

Reavell launches new nitrogen boosting system

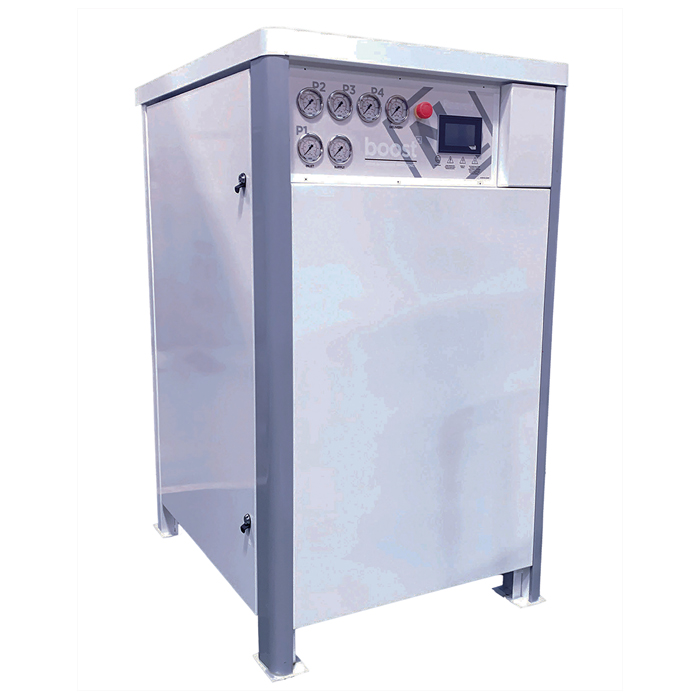
High-pressure compressor manufacturer, Reavell, part of the Ingersoll Rand Group, has launched Boost, a plug-and-play range of four nitrogen boosters.

Designed for easy integration with any nitrogen generation system, the four models (H075, H110, H150 and H185) deliver up to 350 bar pressure outlet and flow rates up to 56 m3/hour on the H185 model.

On-site nitrogen generation has been gaining popularity over recent years, using existing compressors to convert air to guaranteed purity nitrogen. The process can save operators up to 90 per cent of the cost of bought-in gas with payback in less than two years for a company using liquid nitrogen, or as little as one year where gas cylinders are being used.

Compressor upgrade earns energy-saving bonus for custom design and prototyping specialist

When Fabricon Design Ltd replaced its existing compressor installation with an Atlas Copco VSD+ unit to sustain the air supply of its state-of-the-art CNC machining operation, it also gained the benefit of annual energy savings in the region of 51%. 

Starting life in 1984 as a design-led steel fabrication company by founder and managing director, Mark Bushdyhan, Fabricon Design has expanded over the last 30 years to include rapid prototyping capabilities and full-scale production, with all services embracing the latest advances in fabrication technology. 

New vacuum pump ECODRY 25 and 35 plus – compact, ergonomic, energy-efficient

Leybold strengthens the trend towards smart solutions in research and laboratory applications

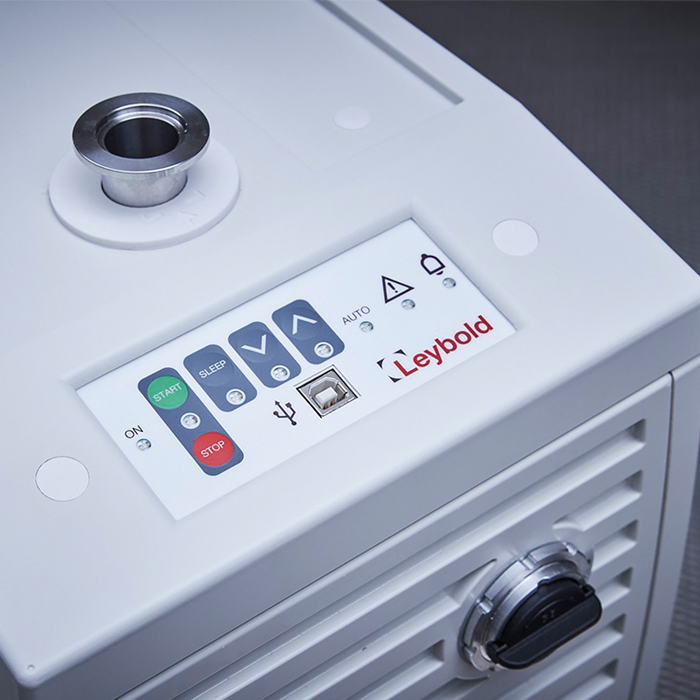
Leybold expands its ECODRY plus product family of dry multi-stage Roots vacuum pumps for laboratory, research and development and analytical applications. The current ECODRY 40 and 65 plus models are now joined by the new, smaller pump sizes ECODRY 25 and 35 plus. Leybold thus completes its range of quiet, low-maintenance and economical fore-vacuum pumps and fills the gap between SCROLLVAC 18 plus and ECODRY 40 plus.

Eaton’s new CMT mobile valve section increases design flexibility and reduces valve bank size with two-service control capability 

CMT expands the CMA advanced mobile valve family

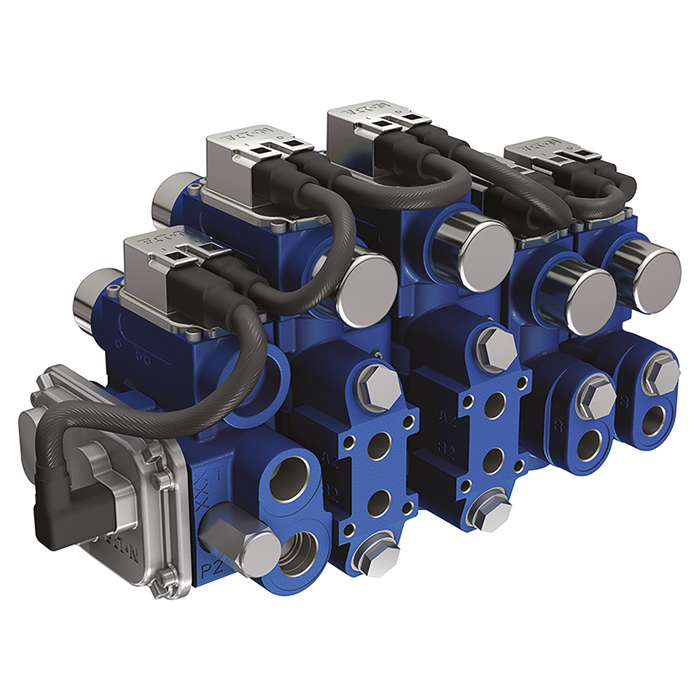
The power management company Eaton has announced the launch of the CMT mobile valve section, a streamlined new section option for the CMA advanced mobile valve. With the capability to control two bidirectional services from one section – an industry first – the CMT valve section increases design flexibility and reduces CMA valve bank size, weight and overall system cost.

Coatings Cut Pump Energy Costs And Carbon Emissions 

Studies collected by the Hydraulic Institute and Europump* reveal that pumping systems account for nearly 20% of the world’s electricity energy demand and from 25 – 50% of energy usage in certain industrial plant operations.  This highlights the significant potential that exists to cut a company’s running costs and put a dent in its carbon footprint too by maintaining or improving pump efficiency.

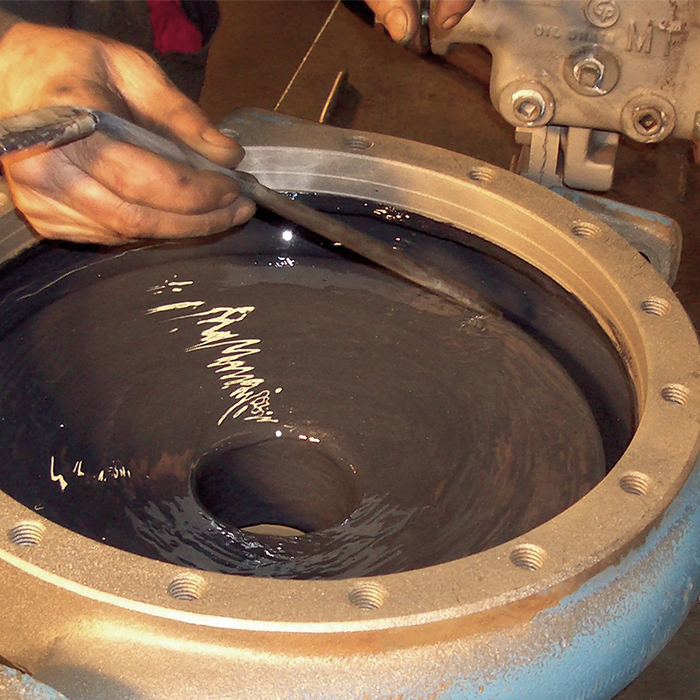
There are several ways to improve the energy efficiency of an industrial pump and the application of a protective coating is one of easiest and most effective.  This is typically a ceramic reinforced epoxy that can extend the life of new pump components and restore the worn surface of old ones.  They create a sacrificial and renewable working surface, protecting the structural integrity of the original substrate.

Castings impellers and volutes all wear due to corrosion, erosion, cavitation and mechanical damage but all these outcomes can be significantly delayed or prevented with the application of a protective coating.  The time it takes to apply is much lower than other remedial methods, such an installation overhaul and impeller trimming and it also achieves the shortest return on investment, typically 4 – 12 months.

30% energy reduction

A UK automotive manufacturer provides an excellent illustration of what can be achieved.  To demonstrate potential gains in pump energy costs a 22kW ELPO pump, used for handling process water, was selected for analysis and it was found to be under-performing by a minimum of 30% against the manufacturer’s original test data. 

The unit was then dismantled and all components examined for wear.  The pump was heavily corroded and pump impeller worn, burred and imbalanced.  The mechanical seal had seized and the pump was out of alignment with the motor.  The volute was cut-water worn, the bearings showed evidence of fretting and corrosion and the motor was not inverter rated.

All components that required coating were first steam cleaned to remove any residue and salts and then bead blasted to achieve a surface roughness of 75 microns.  LOCTITE® 7515 was used to pre-treat the substrates to prevent corrosion and improve adhesion between the metal parts and the polymer composite coating. 

Next, LOCTITE 7177 was applied as a ‘hold coat’ to smooth the surface imperfections and provide a key for the thicker layers required to return the pump to its original dimensions.  A ‘build coat of LOCTITE 7226 was then used to replace many years of wear a create tough surface, resistant to future wear. This was followed by another coat of LOCTITE 7177 to achieve a finish that would reduce friction within the pump and improve its energy efficiency. 

The pump was then fitted with new bearings and both oil and mechanical seals. The impeller was dynamically balanced, the pump re-assembled and a new 22kW high efficiency motor fitted. Motor and pump were finally installed on the bedplate and laser aligned. 

The second performance test was then conducted and the results were outstanding.  The remedial work had restored the pump to original specification, increasing its efficiency by 30%.  The cost of the repair amounted to £5,542.  But offsetting this, in the first year alone, was an estimated energy reduction of £3,936.  This was calculated at £0.08/kWh at 12 hours per day with an 80% load.

The ‘before’ and ‘after’ analysis from other manufacturing companies confirm similar findings.  One reported a 19.9% energy efficiency increase with 4.55 months payback and a carbon emission saving of 10.2 tons per year and another a 12.67% energy efficiency boost, a 5.11 months payback time and carbon savings of 49.5 tons per year.

Ceramic reinforced epoxy coatings are available in a choice of grade for fine particles through to coarse and also specific products for pure chemical attack, corrosion and high impact. 

For more information on the LOCTITE® range and advice on surface treatments in general, please visit our website:
www.henkel-adhesives.com

GET TO KNOW JT TOOL & PLANT HIRE LTD

JT Tool & Plant Hire Ltd is a fast growing tool hire service situated in the heart of London.

 We pride ourselves in providing outstanding customer service to our customers by putting their needs and demands first. Offering Access Support, Handling, Air Tools and Compressors, Cutting and Grinding, Heating Cooling and Drying systems for hire.

Our aim is to go above and beyond the requirement of our customers in order to allow for the smooth and efficient progress of their projects by providing a wide range of tools on demand.

Kings Boiler Hire Work Tirelessly Through The Covid-19 Pandemic

King’s Boiler Hire have worked tirelessly throughout the COVID-19 pandemic keeping hospital, care home and food processing clients running during this difficult time.

Offering boiler units ranging from 1,500lb/hr to 17,500 lb/hr with fast, Nationwide delivery available 24/7,  King’s Boiler Hire is the UK’s No.1 choice for emergency boiler hire.

SKF factories to be carbon neutral by 2030

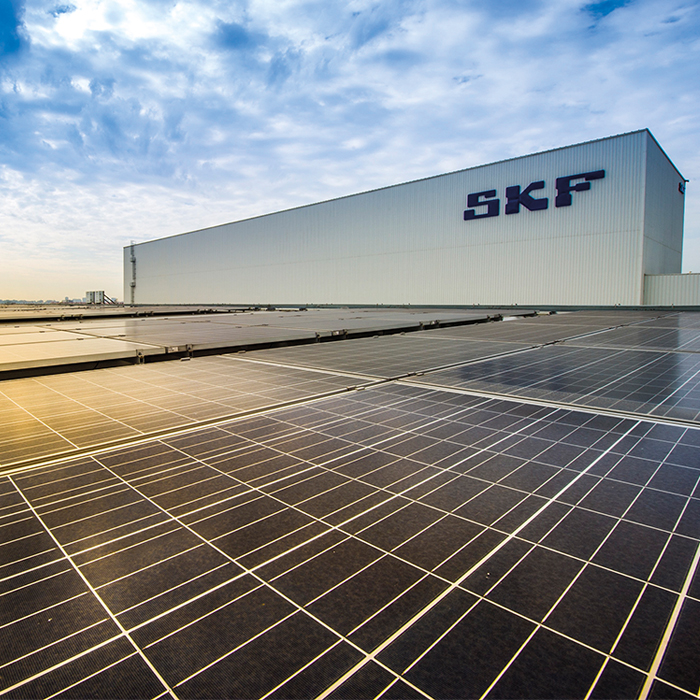
Since 2015, SKF has decreased its manufacturing carbon footprint by 36% and is already operating two carbon neutral factories. Today, SKF announces its aim to achieve a fully carbon neutral manufacturing footprint by 2030.

The 2030 target will cover SKF’s own manufacturing operations, i.e. SKF’s scope 1 and 2 emissions. It will be achieved by a combination of process improvements, energy efficient machinery, and procurement and generation of renewable energy. As a last resort, SKF may also purchase high quality carbon offsets.

This website is owned and operated by: MSL Media Limited

msl logo
www.mslmedialtd.com

Co. Number: 05359182

© 2005 MSL Media Ltd. All rights reserved. E&OE

ems logo mobile