Brammer Buck & Hickman launches new Bore and Keyway Machining Service


Buck & Hickman, the UK’s leading supplier of industrial maintenance, repair and overhaul (MRO) products and services, has launched a new fast and flexible Bore and Keyway Machining Service.

This latest addition to the company’s range of engineering services has seen new bore, keyway and grubscrew machinery installed, operated by experienced in-house engineers. Now, Brammer Buck & Hickman can rework products to suit customers’ specific requirements and within a short time frame.

The new Bore and Keyway Machining Service encompasses horizontal and vertical adaptations. The service that is expected to have the greatest demand is machining customer bore and keyways into pilot bored products such as sprockets and couplings. Sprockets are stocked either pre-bored to receive a taper lock bush, or as pilot bored versions that can be machined with multiple bore sizes. In addition, a bespoke service is offered enabling modification to off the shelf products.

Darren Smart, Category Director - MRO at Brammer Buck & Hickman, commented: “Whilst we have been providing a basic Bore and Keyway Machining Service to customers, up until now this has been outsourced. By investing in state-of-the-art machinery, and staff training, we are delighted to bring this service in-house, for a far more flexible service and a considerably faster turnaround. We can now meet customers’ bespoke requirements and specific tolerances, regardless of whether it is non-standard or has a slightly different fit.”

The new Bore and Keyway Machining Service joins Brammer Buck & Hickman’s range of engineering services which include specialist workshop, gearbox repair and other engineering services geared towards saving customers money.

Brammer Buck & Hickman is part of the Rubix group, Europe’s largest supplier of industrial MRO products and services. For more information, please go to uk.rubix.com/en/service/engineering-services


Snickers Workwear Trousers – More Than Fit For Purpose

Six Work Trouser families to satisfy every need on site - sustainably.

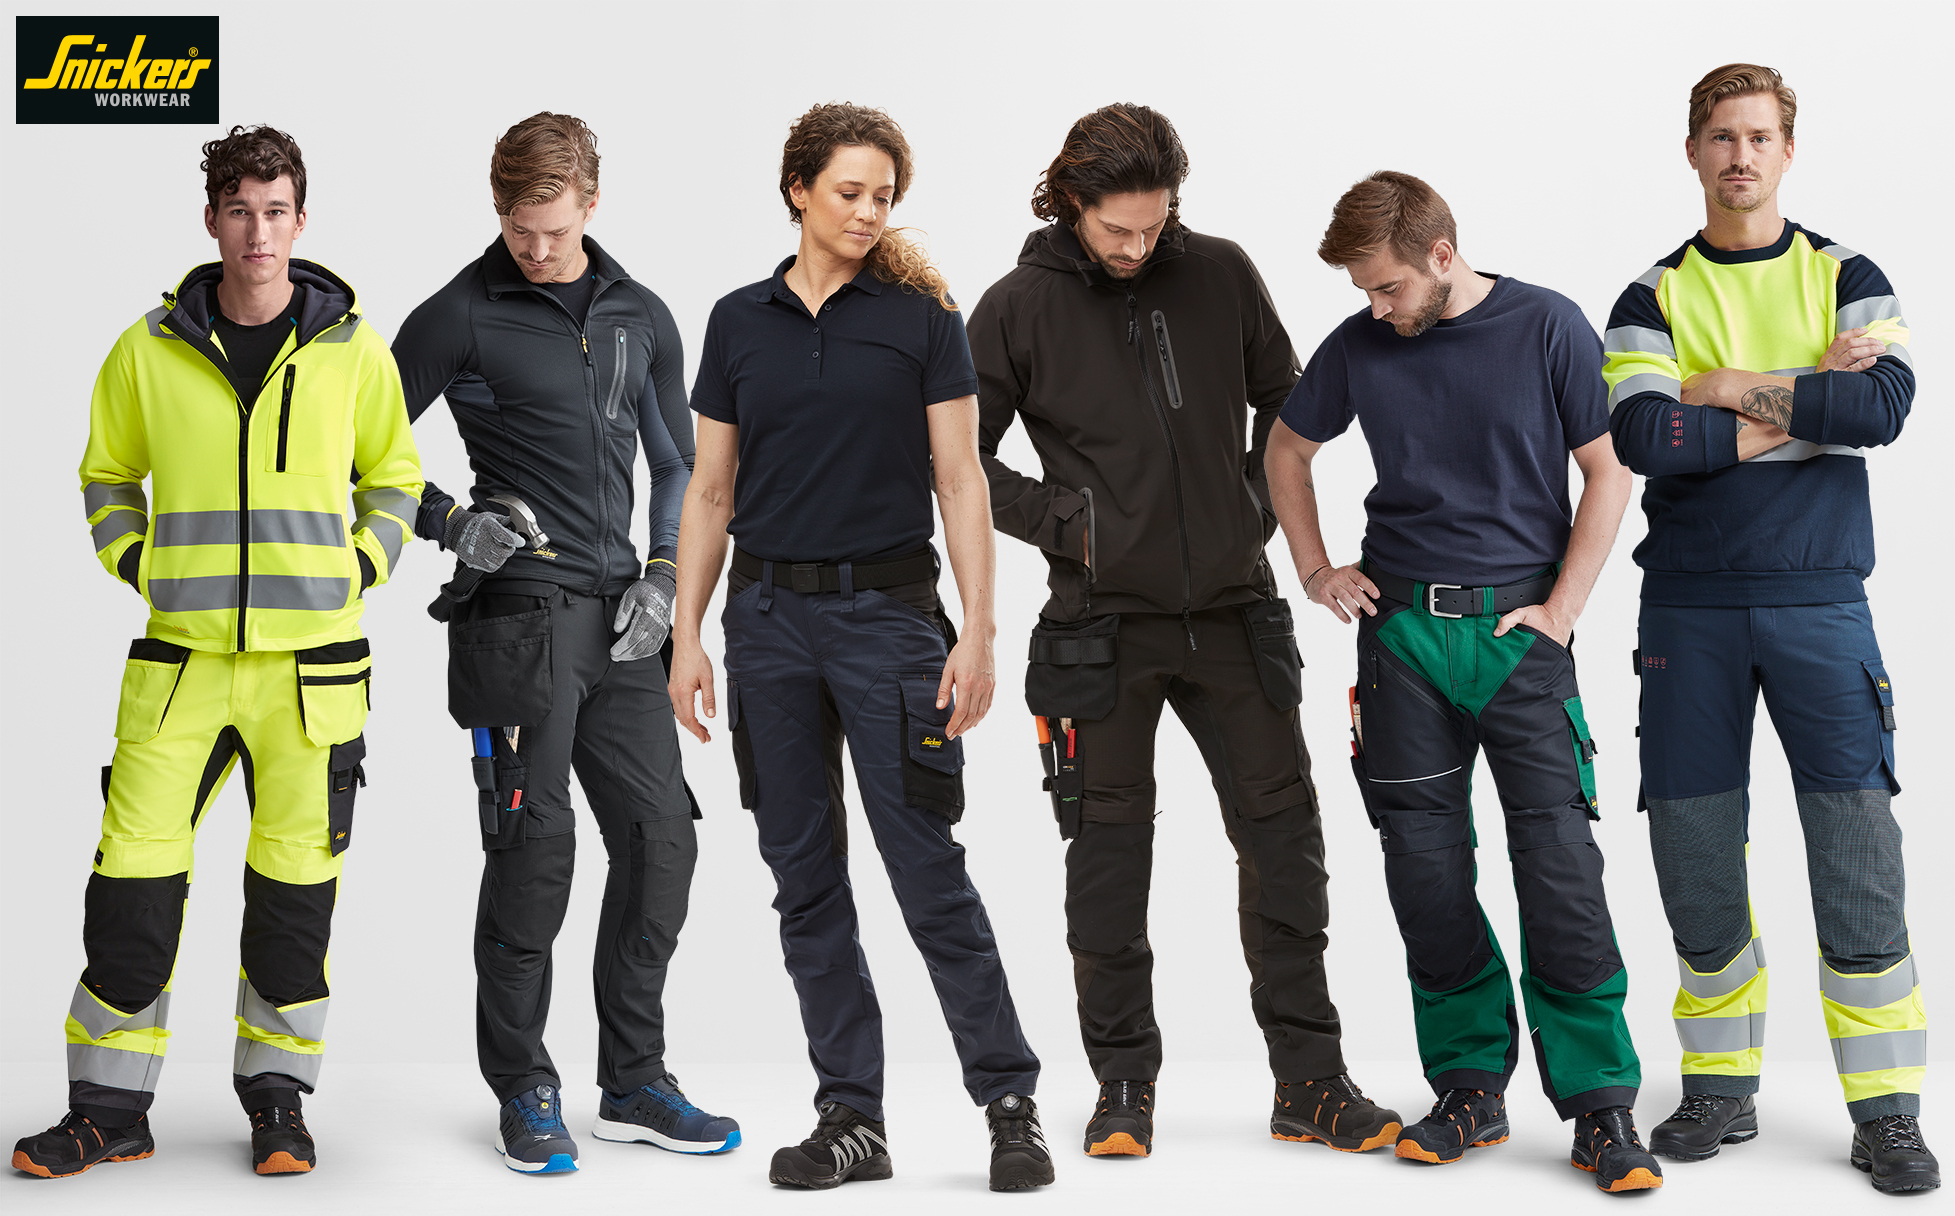
 Snickers Workwear’s trouser families are suited to any kind of work on site. Delivering maximum functionality, comfort, protection and mobility they’re the products of choice among discerning professional tradesmen and women. For them, sustainable, street-smart, body-mapping clothing are key parts of their product choices.

Hi-tech fabrics, functionality and fit are the hallmarks of these market-leading products. The AllroundWork trousers are ready for any kind of work in any trade. FlexiWork trousers deliver superior freedom of movement. While LiteWork trousers keep you cool, dry and ventilated.

Then there’s RuffWork trousers, reinforced and tough for the roughest work on site. ProtecWork protective wear for hazardous environments and certified High-Vis trousers when personal visibility on site is a priority.

work environments.

Snickers Workwear Trousers also deliver certified protection with the patented KneeGuard System for greater flexibility, comfort and durability. It’s what makes them the optimal choice for craftsmen and women who need to get every job done comfortably and sustainably on site. 

 Getting information on the Snickers Workwear trouser families is eay. You can call the Snickers Helpline on 01484 854788, checkout the website at www.snickersworkwear.co.uk or email This email address is being protected from spambots. You need JavaScript enabled to view it.

Water jetting standards get WJA Audited Member boost

The Water Jetting Association has introduced an Audited Member programme giving its members a powerful new opportunity to promote the  standards they set to customers.

The initiative gives users of water jetting services greater assurance that contractors displaying the Audited Member logo meet the WJA’s high standards.

It has been made possible by the introduction of an audit procedure that requires new and renewing members to provide more information and evidence to show services are aligned with WJA codes of practice.

David Malin, Chairman of the WJA Technical Committee, whose members have been overseeing the development of the auding procedure, said: “We’re excited by the opportunities presented by our Audited Member programme.

“It’s going to help the WJA safeguard trusted water jetting standards and, thanks to the quality of the data we’re gathering, will play a key role in helping us to raise them over time.

“Equally important, also, is the opportunity it provides members to promote their services, and make the most of the advantages of being members of the WJA.”

Companies and organisations that use water jetting services, along with regulatory bodies, look to the WJA to set and uphold vitally-important safety and technical standards, said David Malin.

He added: “At the same time, our members join the WJA because they share our values and know customers will be assured by their association with us. The Audited Member programme will help us achieve both outcomes.”

The WJA has now added a range of new questions to its application forms for new members and for companies renewing their membership.

These are designed to extend the amount of information the WJA gathers about the safety and technical standards and processes companies work to, including equipment management and training.

The auditing process is closely aligned to standards detailed in the WJA’s codes of practice – the Blue Code for high and ultra-high water jetting, the Red Code, for use of water jetting in sewers and drains, and the new Purple Code, for pressure washing.

It also requires members and renewing members to abide by the principles laid down in the WJA Charter of Professional Conduct, covering issues that include professional behaviour, competence, incident investigation, and equality.

High and ultra-high pressure water jetting contractors – under the C1 and C1P (Provisional) categories – have been the first to undergo the auditing process. Auditing for members and prospective members in C2 to C6 categories will be rolled out over time.

All members who pass the auditing process will be allowed to display an ‘Audited Member’ logo on their websites, and promote the enhanced status they have achieved to customers and prospective customers.

Development of the auditing system has been led by Jeff Haigh, a WJA Ruling Council member and a qualified auditor.

Under the auditing system, all the new information provided in application forms is being carefully examined. Gaps or inconsistencies are resolved with applicants. Only then can the applications move to the next stage in the approval process.

The WJA also retains the option of carrying out visits to work sites or to company offices as part of the auditing process.

The WJA is grateful for the patience and cooperation of members during the introduction of such a fundamental new programme, said Jeff Haigh. Learning would be fed into later phases of its roll-out.

He added: “This is designed to be a positive process. The WJA wants to support applicants at every stage, sharing information and expertise that will help them with their applications, and to meet the standards we all want to achieve.”

www.waterjetting.org.uk
New Electric and Diesel-powered Hydraulic Power Packs for Portable Machine Tools

Enerpac announces the new PP-Series electric and diesel-powered power packs to supply hydraulic flow to Enerpac portable machine tools, including flange facing machines, clamshell cutters, hot tapping machines and decommissioning tools. The hydraulic power packs are also compatible with other brands of portable machine tools.

The Enerpac PP-Series includes a total of four hydraulic power packs comprising two electric and two diesel powered models. Variable pumps within the power packs allow pressure and flow to be adjusted for specific applications.

Electric PP-Series Power Pack


Portable machine tool operators with access to an electric power supply can choose between the electric powered hydraulic power pack 11 or 15 kW models - each available with a choice of voltage options for use throughout the world.

Machine Specific Control Pendants

Many manufacturers of hydraulic power packs provide a simple general-purpose control pendant as standard with each unit. Although this is adequate for simple machining tools, it is of little use to control other machine types such as gantry mills, or 3-axis milling machines.

To meet these different applications, customers buying an Enerpac Electric PP-Series Power Pack can get exactly what they need. The range of pendant options offered provides a perfect match to suit the specific machine tool. In addition, for operator safety emergency stop buttons are provided on the power pack and the control pendant.

Diesel PP-Series Power Packs

For working in remote locations, customers have a choice of 19 and 44 kW units. These more powerful power packs are the optimum choice for larger machine tools used for operations such as hot tapping and decommissioning.

Both the Enerpac Diesel PP-Series PP19 and PP44 units are diesel powered and meet the EU Stage V and EPA tier 4 final regulations for emissions. Each includes a 50-liter diesel tank, which, in the case of the PP44, can provide up to 12 hours run time at maximum torque. Also included in the diesel power packs is a spark arrester for added safety in explosive environments.

Unlike the electric units which work with pendants to provide control, the PP19 and PP44 power packs require a separate hydraulic control panel and machine specific hose kits. The hydraulic control is connected to both the machine tool and the hydraulic power pack. The control panel houses all the controls needed for a specific machine’s requirement.  In addition, the Diesel PP-Series power pack features a pressure-less switch to remove pressure and flow.

Choice of Hose Kits

A 10-meter hose kit is supplied as standard and longer hose kits are available as accessories for single-supply, dual-supply and triple-supply applications. Triple supply hose kits allow three hydraulic motors to be connected to the power pack simultaneously, along with spindle control the operator can also select the required axis (x or y) from the pendant.

Machine operators choosing an Enerpac Electric PP-Series Power Pack can also benefit from an optional cart to enable easy positioning and storage within a workshop environment.

Site Ready

For ease of handling and deployment, the Enerpac PP-Series electric and diesel-powered power packs are enclosed within a protective frame and Forklift truck and vertical lift points

For more information on the Enerpac PP-Series electric and diesel-powered power packs, visit www.enerpac.com.

Meantime Brewing Replaces Boiler and Expands Capacity with Babcock Wanson

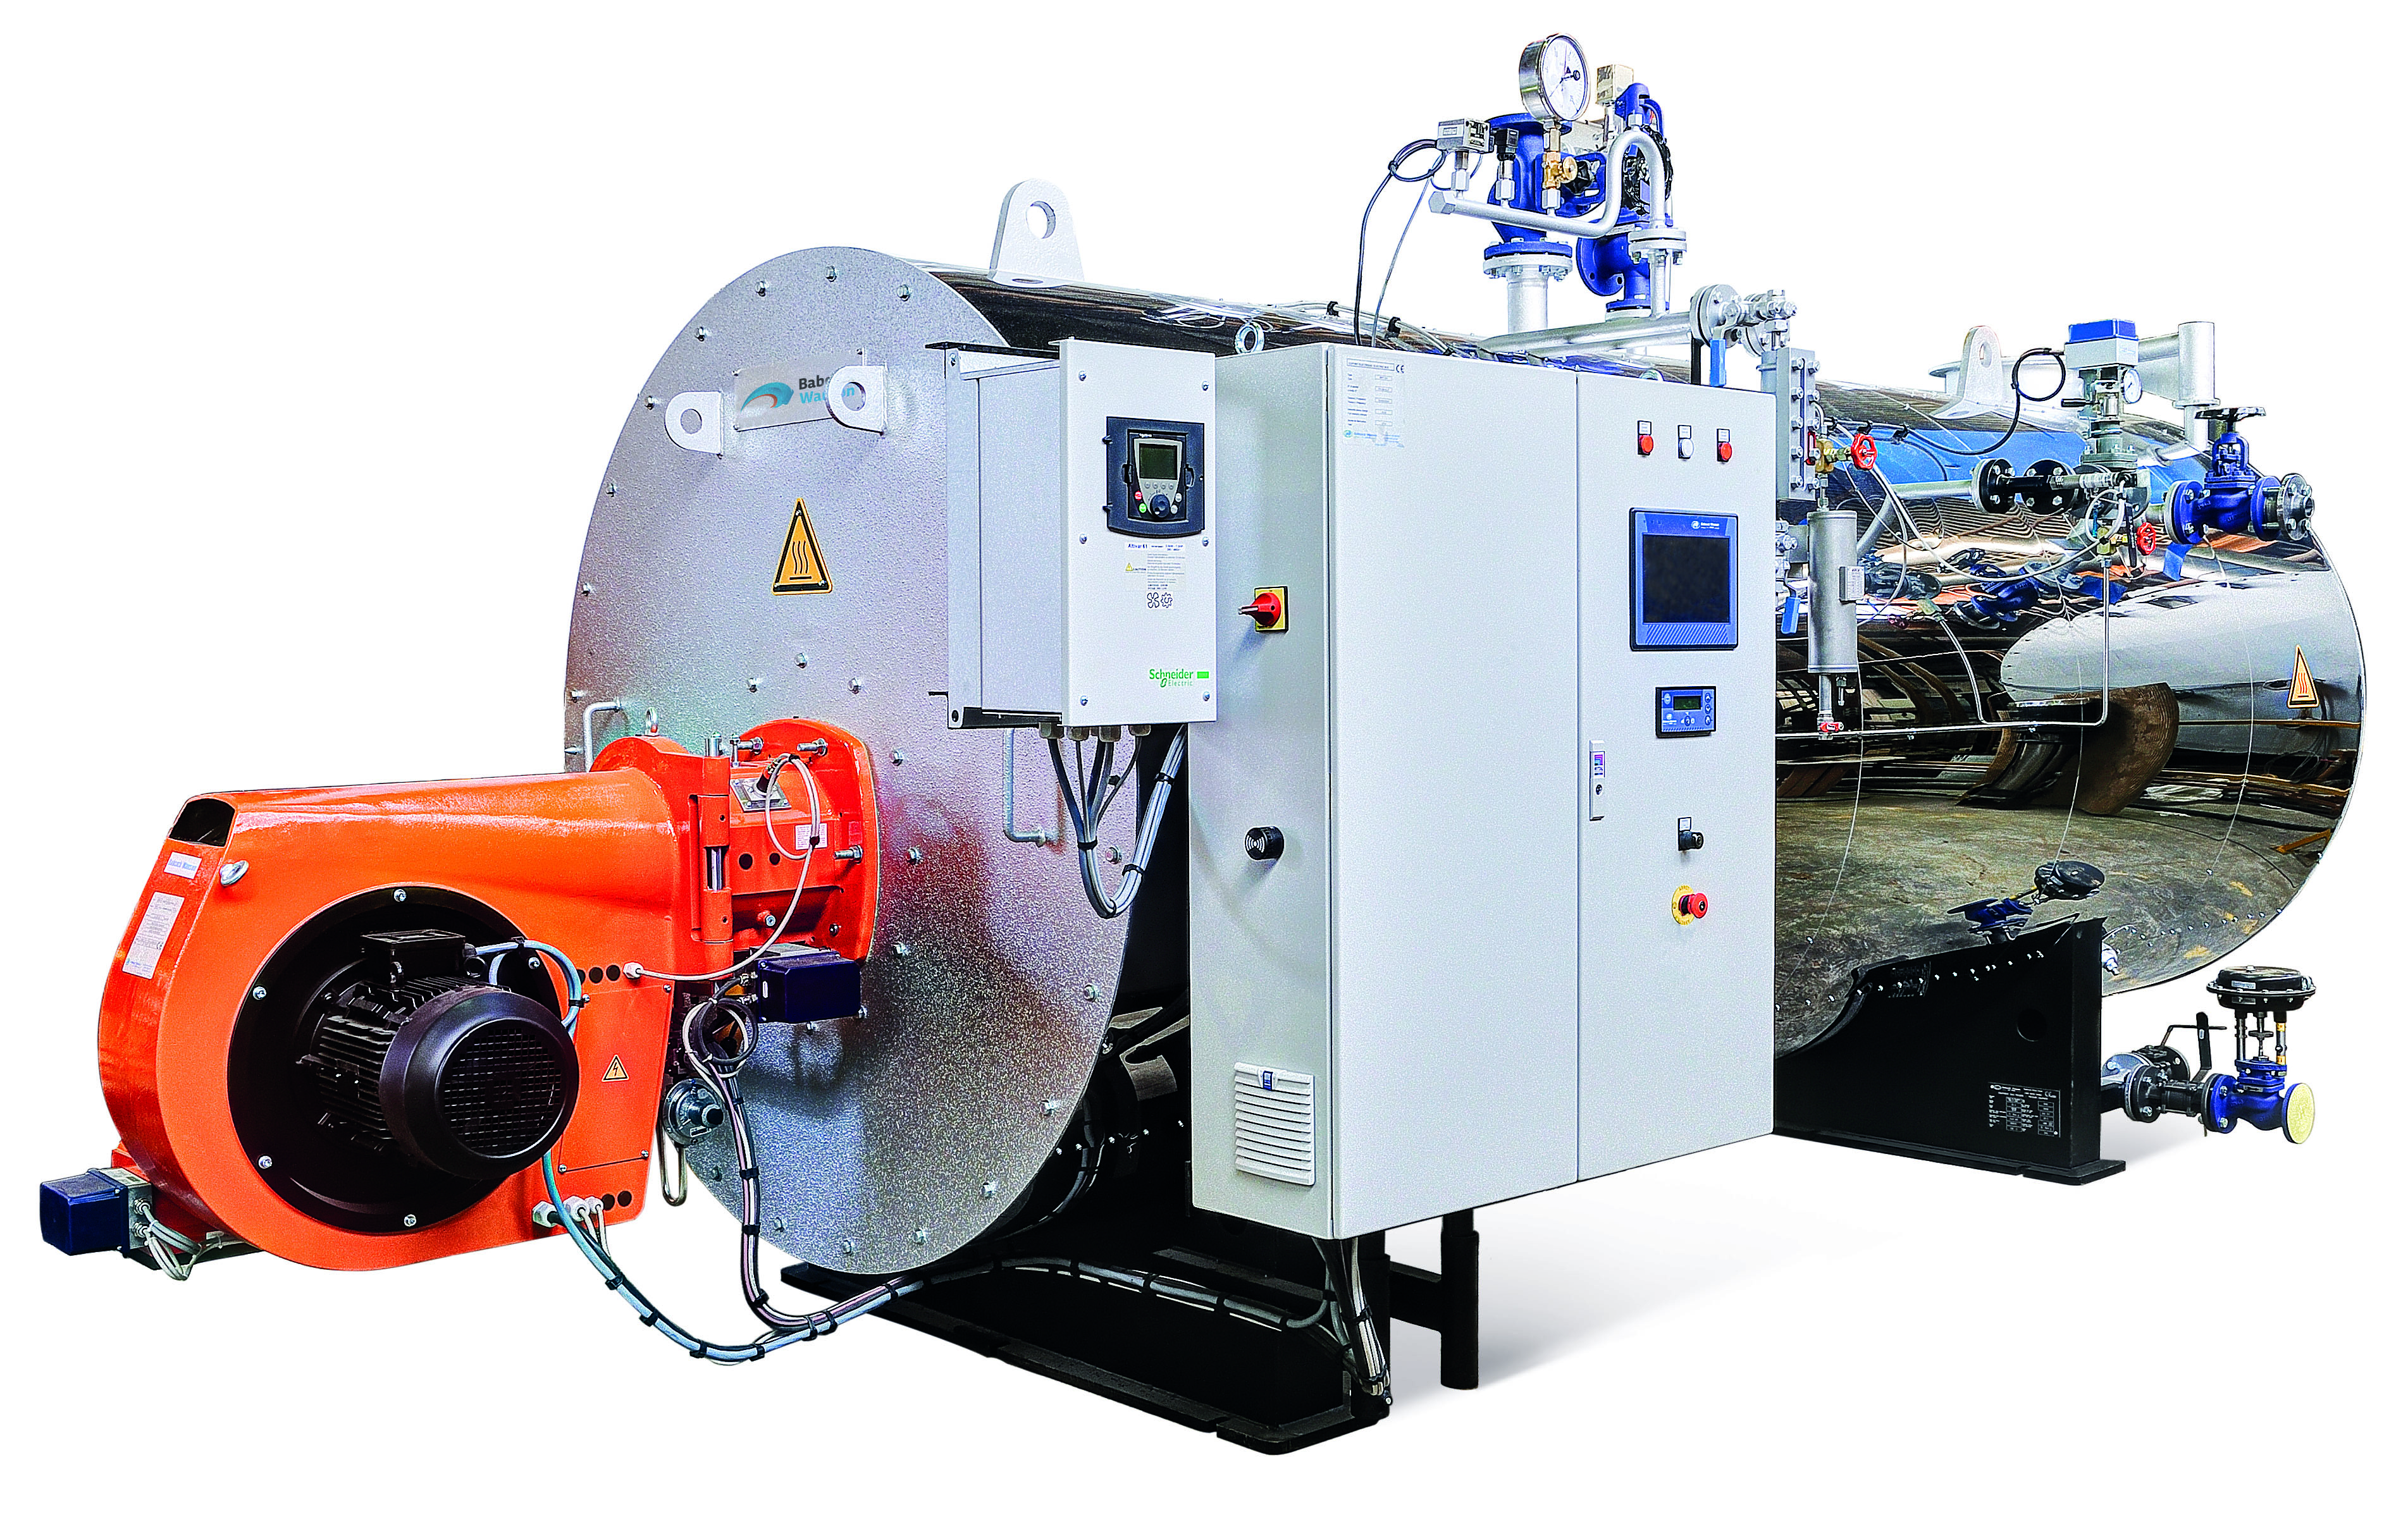
A Babcock Wanson BWD40 Fire Tube Boiler has been installed into Meantime Brewing’s Greenwich, London site, which is used in multiple aspects of brewery operation, from wort production through to packaging line operations. The 4 tonne BWD40 is a replacement for the existing 2.5 tonne boiler, which had come to the end of its working life.

Established in 1999, and based in Greenwich, London, Meantime Brewing Company is part of Asahi UK and has earnt a reputation as a modern pioneer of craft beer in the UK. It has an exciting line-up of core beers such as London Lager and Anytime IPA and innovative collaborations and seasonal beer releases throughout the year. 

In a recent refurbishment of its Greenwich site, to both increase capacity and reduce its carbon footprint, Meantime Brewery appointed industrial process heating specialist Babcock Wanson to undertake the boiler replacement works. This included supplying the BWD40 Fire Tube Boiler and carrying out all the mechanical and electrical works as part of a turnkey solution. Babcock Wanson developed the plans in close consultation with chief engineers from across parent company, Asahi UK, and ensured the site meets BG01 Guidance on the Safe Operation of Boilers. BG01 advises on boiler control technology and how to achieve the safety standards laid out in the HSE’s ‘Safe management of industrial steam and hot water boilers’ document (INDG436).

The Babcock Wanson BWD40 Fire Tube Boiler was chosen as the process heat source for this site due to its high efficiency, long life and low cost maintenance. Efficiency comes as a result of the optimised matching of the boiler shell and the burner, along with advanced burner head geometry which provides stable combustion with near constant efficiency throughout the complete burner modulating range. 

Longevity and reduced maintenance requirements are a direct result of the three pass design and use of a coaxially located furnace tube providing optimum distribution of mechanical stress in operation. This is an important feature for boilers that operate under variable steam load, such as at Meantime Brewing, and ensures long equipment life.

Further benefits of the BWD40 are lower total exhaust emissions. Using Babcock Wanson’s latest Optimo burner, the BWD40 has emission rates of less than 100mg/Nm3 NOx throughout the firing range when burning natural gas, making it one of the best performing burners on the market.

The new boiler in place, with its low NOx emission rates, readily meets the Medium Combustion Plant Directive (MCPD), which covers emissions of sulphur dioxide, nitrogen oxides and dust pollutants to the air. Babcock Wanson assisted Meantime Brewing with the required application for a new MCPD environmental permit, working with a third party who conducted a detailed boiler house risk assessment covering all relevant aspects - including steam, electrics, operations – and produced a written report.

Babcock Wanson offers a complete range of products and services for boiler houses and other process heating needs, from steam boilers, thermal fluid heaters, rapid steam generators and hot water boilers to VOC and odour treatment by thermal oxidation, water treatment or process air heating solutions. The company has extensive experience in the brewing and distilling sectors. 

For more information, please contact Babcock Wanson on 020 8953 7111 or This email address is being protected from spambots. You need JavaScript enabled to view it. or go to www.babcock-wanson.com/product-category/coil-type-steam-boilers/

ENDS


LOCTITE-SPONSORED TEAMS EXCEL AT FORMULA STUDENT 2022

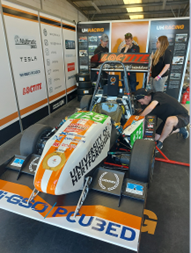
All four university teams sponsored by Henkel and its industry-leading LOCTITE® products finished in top 20 positions at this year’s Formula Student 2022 competition, which took place at Silverstone on 6-10 July. The University of Southampton, University of Hertfordshire, University of Bath and University of Sheffield achieved 9th, 12th, 15th and 17th place finishes in the overall standings, with all achieving top 10 results in individual disciplines.

Formula Student is Europe’s most established educational engineering competition, an event that uses motorsport to inspire students. Backed by industry and high-profile engineers, such as patron Ross Brawn OBE, the competition aims to develop enterprising and innovative young engineers. Each team is tasked with producing a single-seat race car before presenting it to a hypothetical manufacturer, with all going through a rigorous testing process made up of static and dynamic events.

The University of Southampton, which entered its very first electric car in 2022, not only took a highly creditable 9th place overall, but finished 3rd in the design competition and 4th in the cost discipline. Among the innovative LOCTITE products contributing to this fine performance were LOCTITE 3090, a fast fixturing, gap-filling cyanoacrylate adhesive that works well on most plastics, rubbers and metals. The University of Southampton also took advantage of LOCTITE EA 9497 epoxy adhesive, LOCTITE EA 9466 epoxy potting resin paste, LOCTITE EA 9461 epoxy structural bonding adhesive and LOCTITE SF 7414, a blue, high-viscosity, fast-drying paste that allows the visual detection of any movement during the adjustment of parts.

The University of Hertfordshire was not far behind, finishing 12th overall, a result built on success in categories such as cost (5th), business presentation plan (6th) and design (10th). Again using an electric powertrain, the car leveraged the benefits of products such as LOCTITE 770-NC Frekote® as the mould release agent for composite components, all of which the team manufactured in-house. Further products in evidence on the race car were TEROSON® PU 6700, a polyurethane-based adhesive used for bonding composite structure panels to the chassis, while another important product was LOCTITE HY 4070, a fast fixturing cyanoacrylate/acrylic hybrid adhesive that the team used for bonding rubber around sharp composite edges.

Finishing 15th overall was the University of Bath, supported by highly noteworthy finishes in the design competition (6th) and cost category (7th). Based on mission statements for 2022 that included improvements in weight reduction, handling and reliability, the University of Bath tapped into the benefits of products like LOCTITE 770-NC Frekote epoxy mould release agent for advanced composites, LOCTITE Frekote B15 mould sealer, LOCTITE EA 9466 epoxy potting resin paste and LOCTITE SI 5910, a gasketing product for flexible flanges with good resistance to oil and joint movement.

Also managing a top 20 finish was the University of Sheffield, which was 17th overall supported by an impressive 8th place in the design competition. For this year’s race car, the University of Sheffield manufactured its first carbon-fibre monocoque chassis. Among other products, Henkel supplied LOCTITE EA 9497 for repairs to both the chassis and mould, as well as for sealing a number of aerodynamic components. Another important product was LOCTITE HY 4070 instant adhesive for structural bonding.

In addition, the teams deployed a myriad of LOCTITE threadlocking adhesives, gasket sealants, retaining compounds and cleaning products, all of which contributed to a highly successful Formula Student 2022. Plans and developments are already underway for the 2023 race cars.

For more information go to: www.henkel-adhesives.co.uk

Landia aerate the holiday park

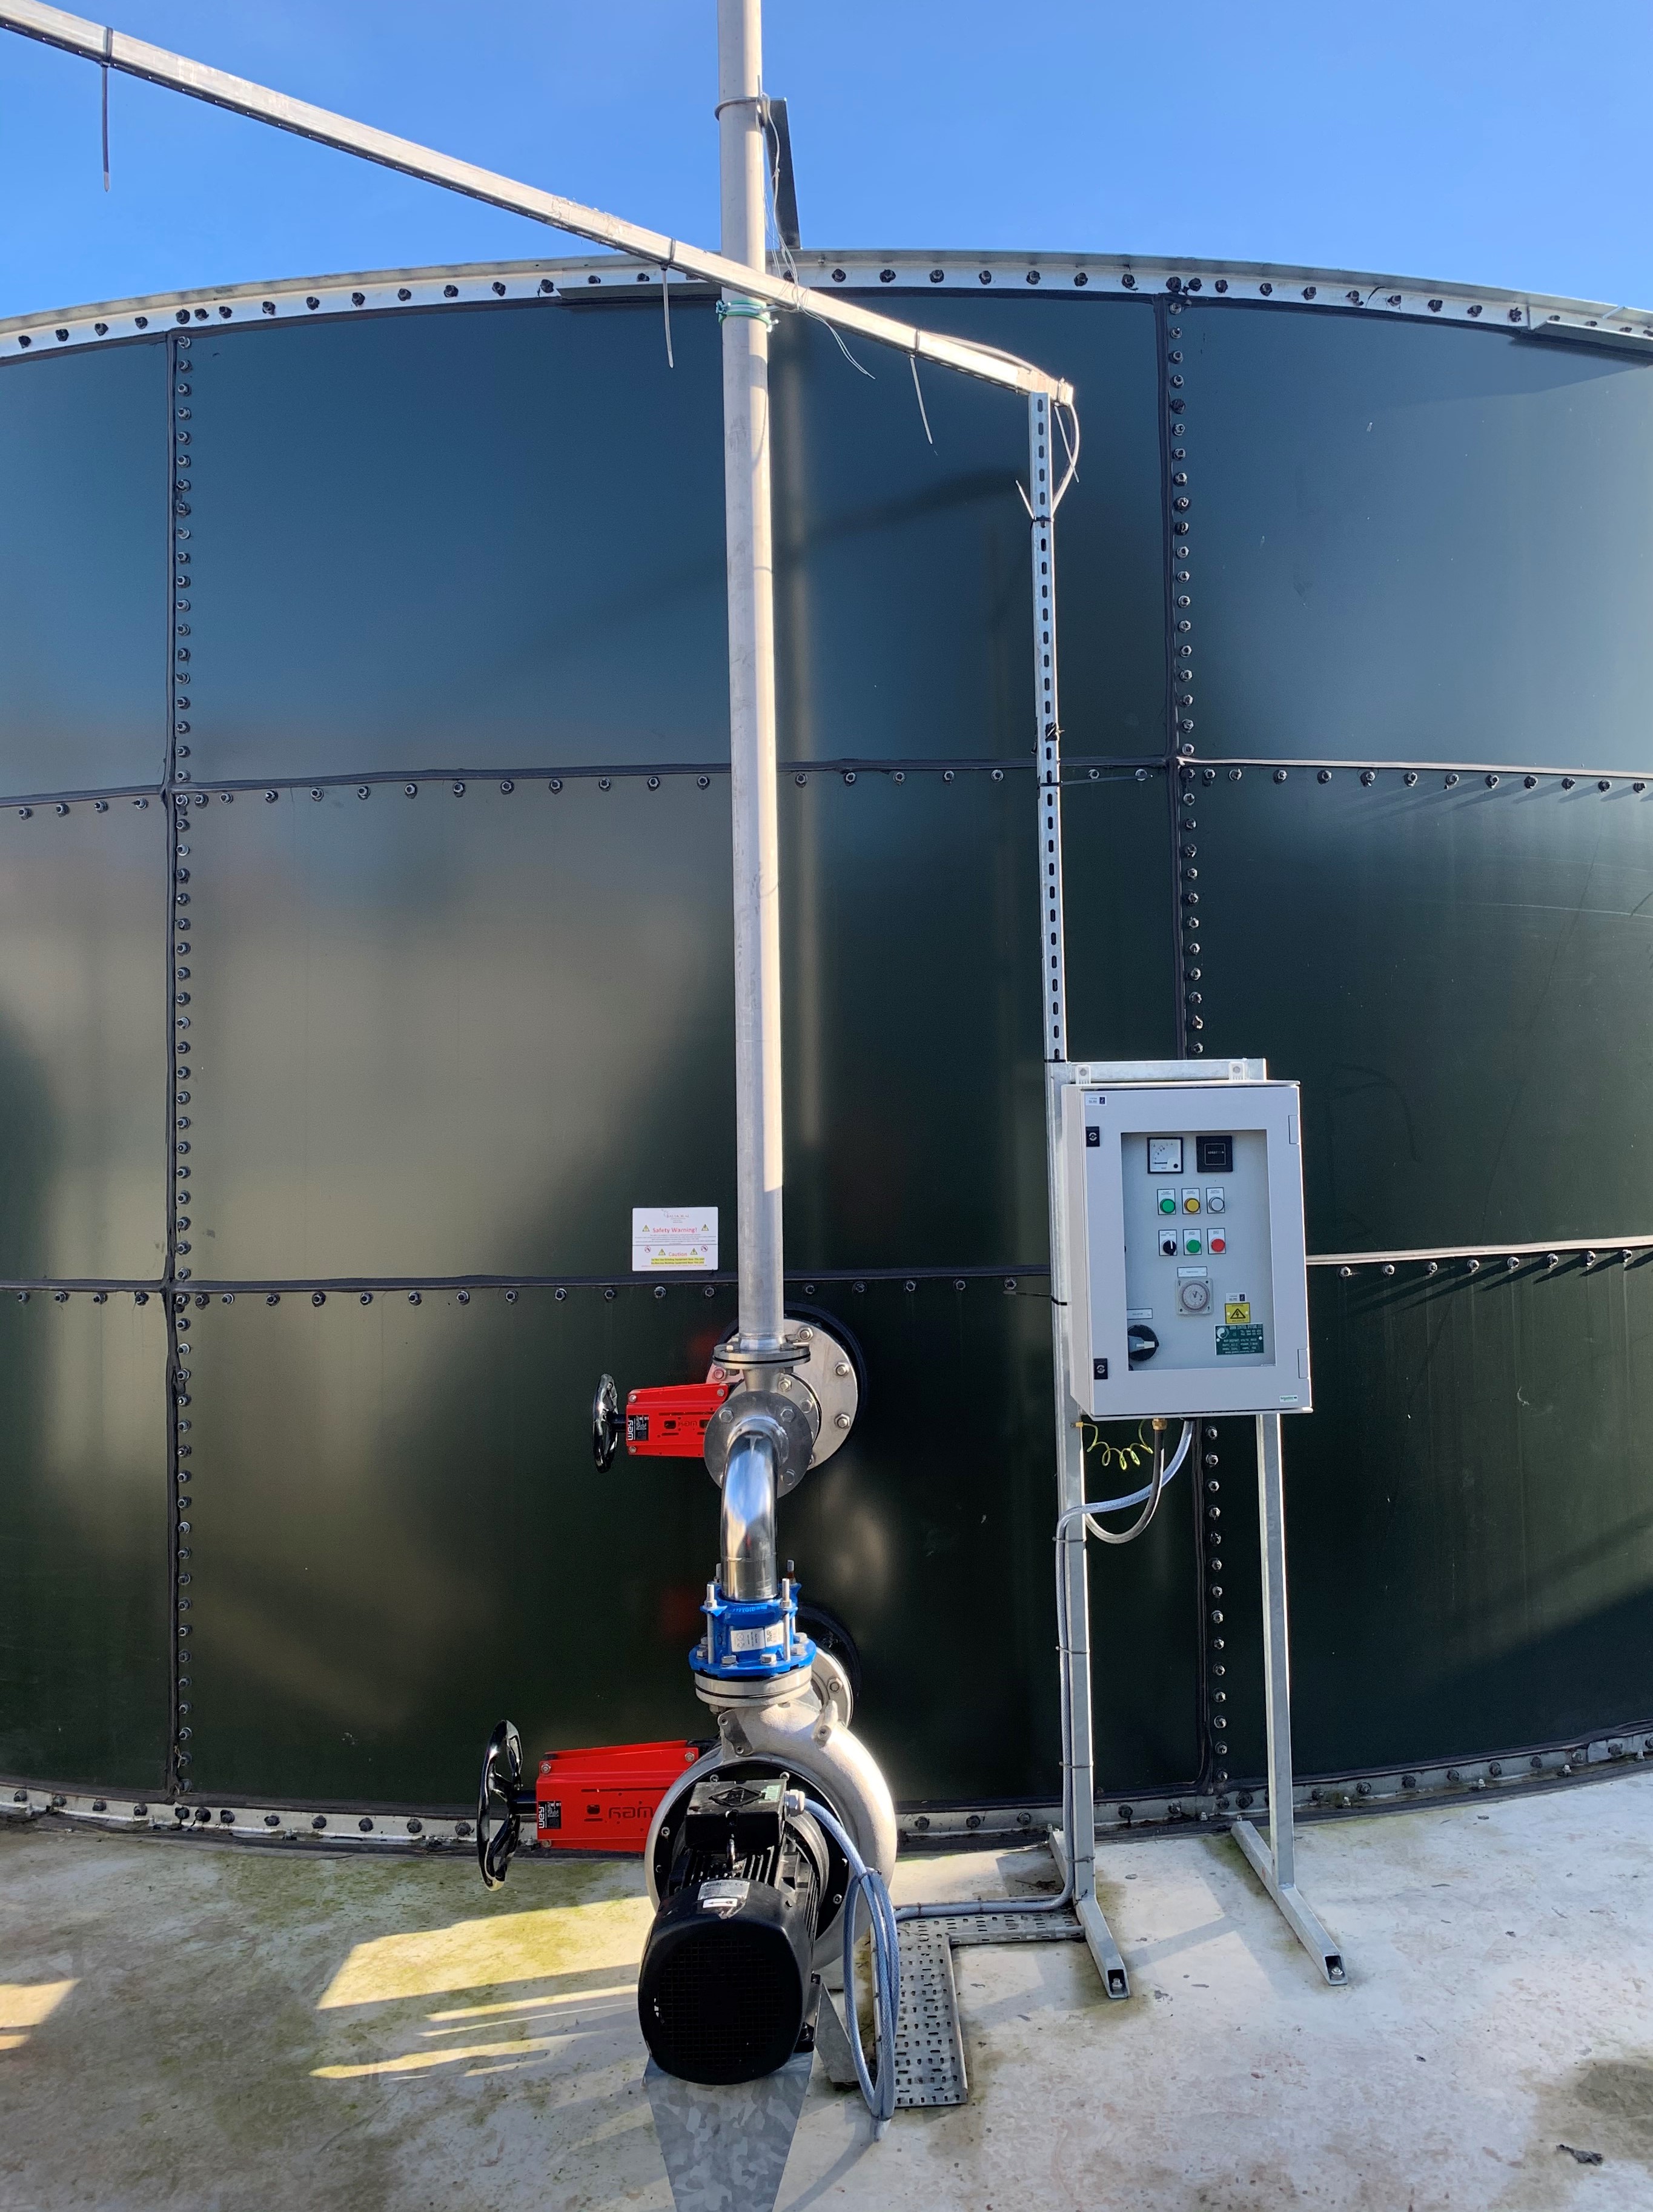
Following three years of successful service by Landia aeration units at one of the UK’s most popular holiday parks, a leading water and wastewater asset management company has introduced an additional Landia unit to one of its customer’s other sought-after destinations.

As well as for the holiday parks it works with, the asset management company has also brought in Landia’s aeration equipment to serve customers in the food and beverage industries, including a dairy in the south west and a drinks manufacturer in Yorkshire.

The Landia AirJets, which mix and aerate wastewater in balance tanks, include the Landia Chopper Pump (invented by the company in 1950) and a venturi nozzle, which together can either reduce or eliminate the need for high-energy use blowers.

This latest order follows Landia’s successful work with Viridian Systems, where at a landfill’s leachate treatment centre, a new mixer has created annual savings on chemicals of around £85,000 ($101,000)

www.landiaworld.com

Ultimo and Additude sign a partnership to support industrial companies in the Nordics with asset management

Enterprise Asset Management (EAM) software vendor Ultimo extends its offering in the Nordics by partnering with industrial solution provider Additude. Based in Sweden, Additude is part of ICT Group, a leading European industrial technology solutions provider. The company offers innovation support, strategic consultancy, SW & HW development and complete IoT solutions for industrial customers. The partnership will benefit asset-intensive companies, as Additude can now offer them a single point of contact for all asset management challenges, helping streamline operation.

Additude offers the Ultimo portfolio as part of its extensive range of software solutions and services for the industrial sector. It can now deliver EAM software that not only delivers asset data but also defines actions to get the most out of the assets. This helps Additude’s customers, typically midsize and large industrial companies in the Nordics, improve asset performance and maintenance efficiency.

Marcel Leeflang, Head of Channel Sales at Ultimo, said: “With our leading Enterprise Asset Management platform, Additude will bring new value to its customers through a fully-integrated APM and EAM offering, which truly improves their asset performance. Our EAM solution can be tailored to the specific needs of each customer. The partnership will also accelerate Ultimo’s growth and enhance our presence in the Nordics, helping us support new customers with their maintenance and asset management challenges.”

Sam Aston, CEO of Additude, commented: “We focus on integrating data and adding value to our customers through smart industry 4.0 solutions. By joining forces with Ultimo, we now cover the maintenance part of the digital transformation and offer a complete solution including virtually-assisted remote maintenance, predictive maintenance and asset performance management. With Additude’s entrepreneurship and long experience in delivering engineering expertise, as well as tailor-made solutions and services for different industry sectors in the Nordics, working together with Ultimo is a logical step. I’m convinced that their wealth of experience in asset management will contribute to the success of our customers.”

www.ultimo.com

www.ictgroup.eu

Rittal Blue e+ S cooling units Cool successor with sustainable DNA

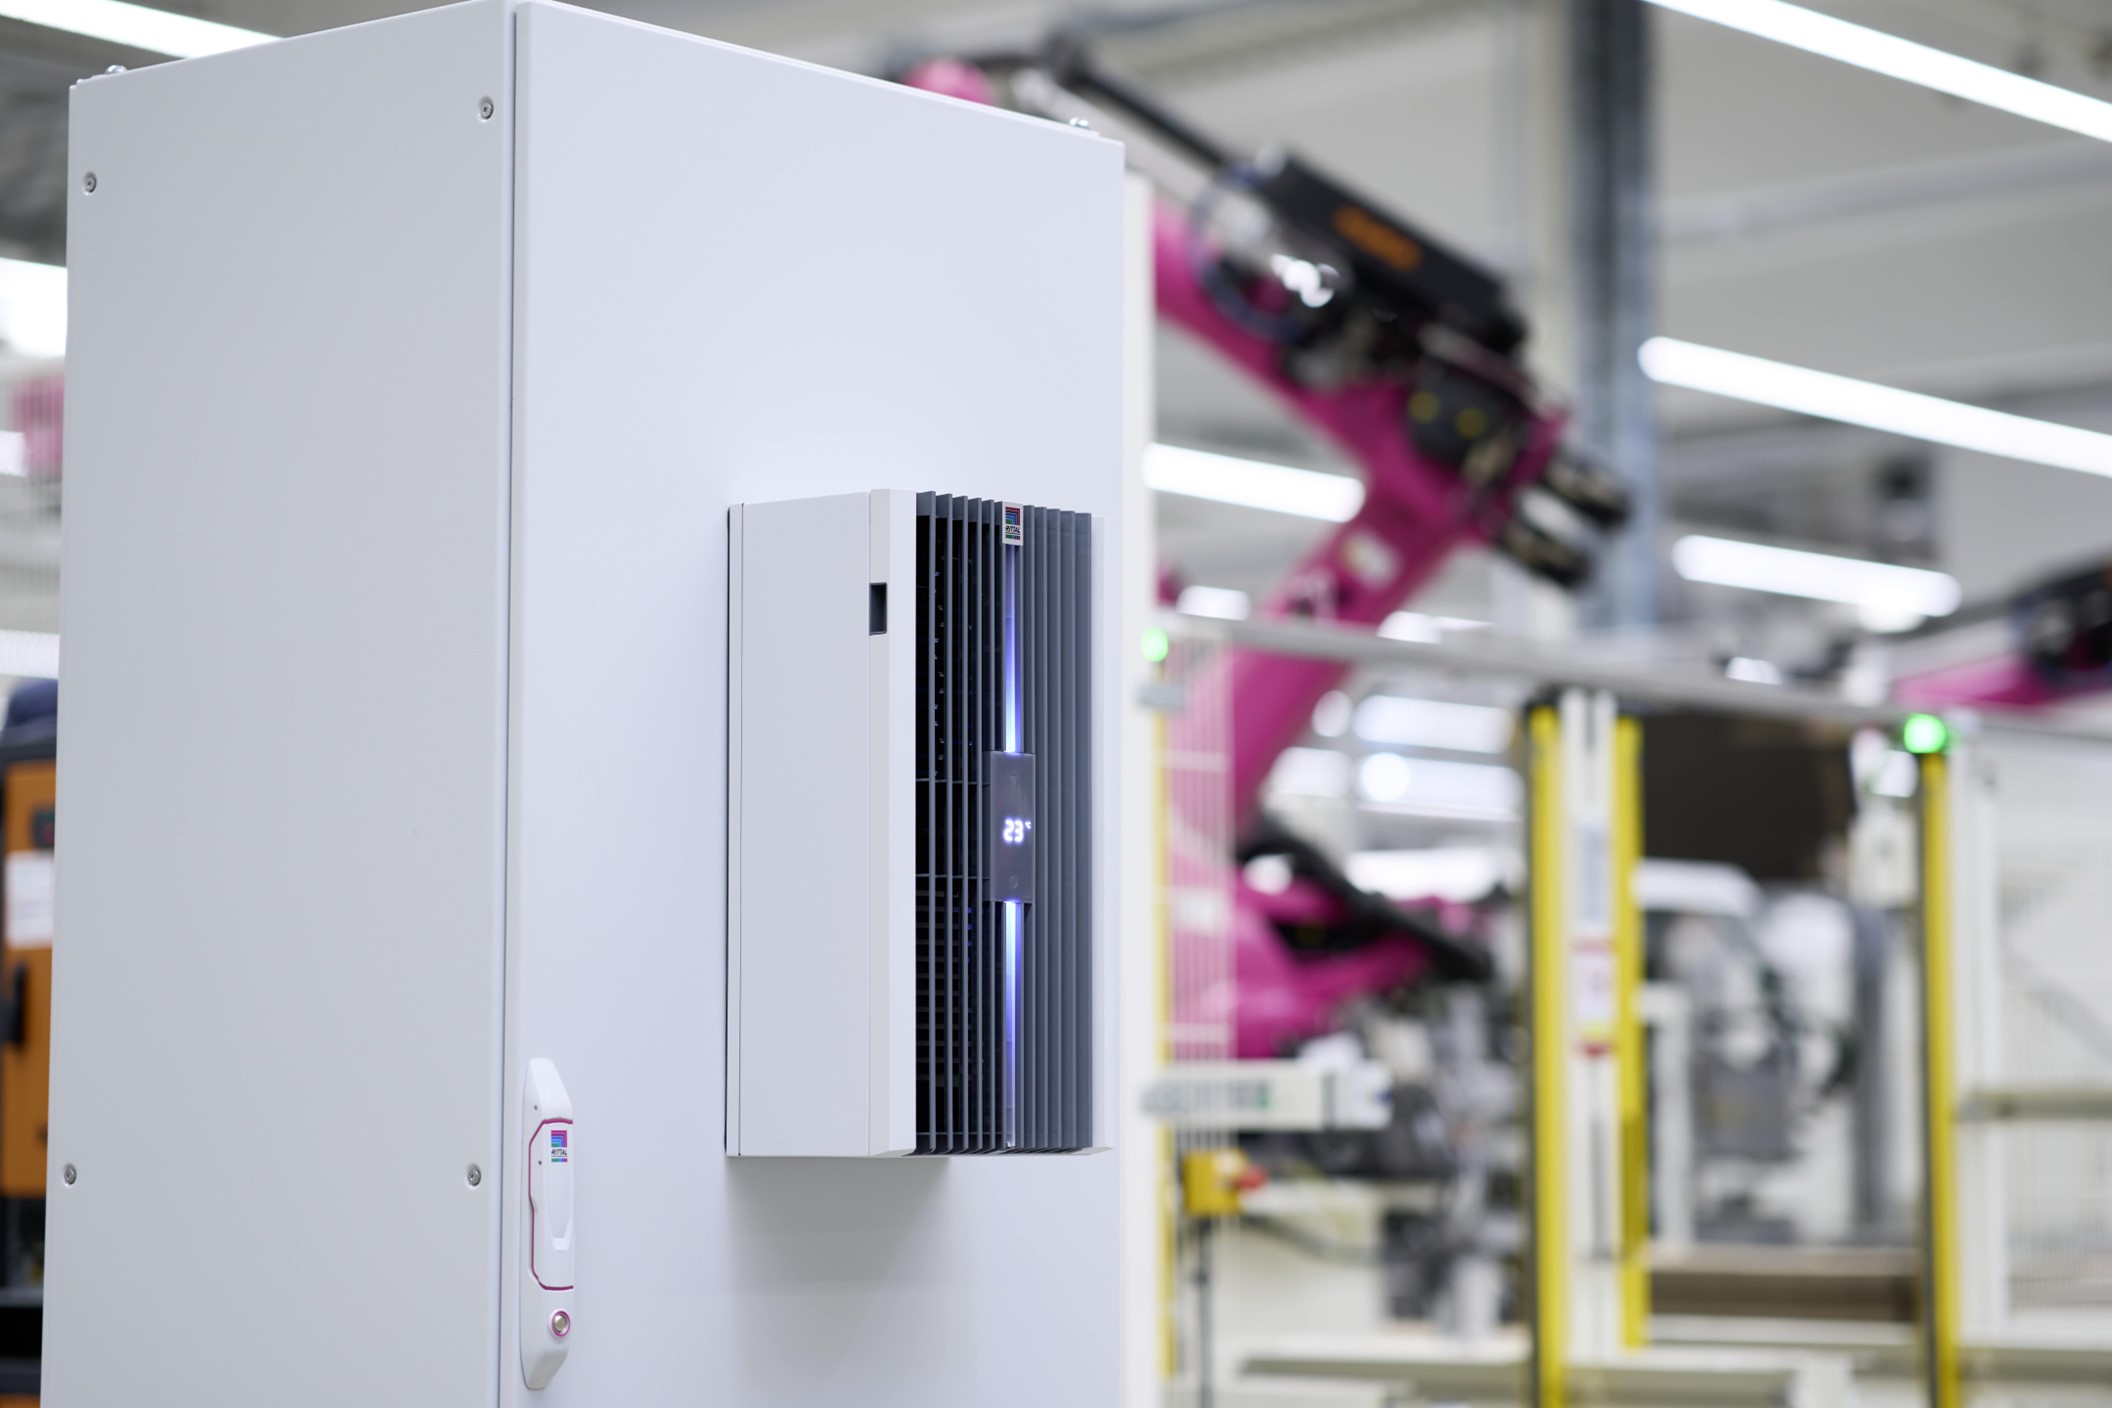
Rittal is expanding its smart cooling unit solutions by adding the new Blue e+ S range. Our latest generation of cooling units with their lower output categories of 300, 500, and 1,000 W have been designed for efficiency, ensuring a smaller footprint and lower costs – just like their “bigger brothers.” So it’s a win-win both for users and for our future.

Solutions that reduce our carbon footprint during production are in high demand. But at the same time, these solutions need to be intelligent and communication-enabled so that they can be easily integrated into digitalised manufacturing environments. Seven years ago, Rittal responded to this demand with its Blue e+ range of cooling solutions and launched extremely efficient enclosure cooling units, which provided on average energy savings of 75 percent. Now we have a new generation – the next generation – but still developed with that same design DNA. These new cooling units with their lower cooling outputs of 300, 500, and 1,000 watts called “Blue e+ S” add to the Blue e+ family and bring with them additional smart capabilities. And furthermore, this new generation offers innovative energy-saving features for the production process.

What’s behind this energy-saving and therefore cost reduction is the technology used, combining a heat pipe with inverter-controlled components. The heat pipe works without a compressor, expansion valve, or other regulating elements and so does not need any electrical energy except to operate the fan. Depending on the thermal energy generated in the enclosure and the current ambient temperature, cooling can be performed with the heat pipe alone. The additional compressor cooling only operates if a large amount of heat has to be dissipated from the enclosure or if the ambient temperature is very high. And what’s more – when it does operate, it is far more energy-efficient than conventional units. This is because the compressor and fans possess an inverter-controlled drive, which automatically adjusts their speeds depending on the requirements. As a result, the temperature within the enclosure remains constant, and the energy efficiency is significantly higher than with other more conventional cooling units.

Staying cool all the time

Alongside energy efficiency, another feature also reduces the carbon footprint: The new Blue e+ S series uses a refrigerant with a GWP (Global Warming Potential) that is 56 percent lower than those used in comparable cooling units. Furthermore, instead of the R-134a previously used, the cooling circuit in the new generation of units now runs with R-513A refrigerant.

Smart communication-enabled capabilities

With their additional smart functions, the new cooling units also help in the digitisation process. With a fully integrated IoT interface as standard, the cooling units can be intelligently monitored in digitalised environments and easily connected to Rittal's new Smart Service Portal. This optimises the service processes and increases efficiency through predictive maintenance. As a result, fewer unplanned downtimes occur which all helps to manage the high cost of production, especially with Industry 4.0 processes.


Production-friendly facelift

These cooling units in the lower output classes have also undergone a facelift. Their most striking feature is an integrated coloured LED light strip. This means that warning messages can be immediately seen, even from far away. A display on the front of the enclosure provides additional up-to-date information. Moreover, the cooling units are equipped with the familiar NFC interface, which enables them to communicate with mobile devices that have the Rittal Scan & Service app installed.

For further information on the entire Rittal range visit  www.rittal.co.uk or check out our linkedin page @rittal-ltd-uk

Industry-leading Speakers Announced at Europe’s Leading Lubricant Exhibition and Conference

 Europe’s leading event for the lubricant industry, Lubricant Expo, has released details of its conference programme for 2022 featuring exclusive insight and leading global speakers.

The three-track conference, taking place on the 6th - 8th September 2022 at Essen, Germany, is free-to-attend and will connect lubricant solution providers with the full range of end-user buyers, as well as the entire chemical and equipment supply chain. The conference has attracted leading experts from global brands to share exclusive knowledge and insight.

Conference attendees can expect to hear both strategic and technical sessions focused on the innovations taking place in the lubricant industry, technologies requiring new, high performing lubricants, the global diverse market and how sustainability and cost remain the two key considerations. There will also be discussions on the current challenges the industry is facing such as the global supply chain issue

On day one (Tuesday 6th September) the conference will open with its first keynote session, ‘What is the Global Picture for Lubricants and How are Sustainability Targets Impacting the Sector and its End Users?’.  Dr David Whitby, CEO, Pathmaster Marketing Ltd will chair the session and Pranav Bhanage, CEO, PETRONAS Lubricants ( India) Pvt Ltd, Maurizio Abbondanza, Sustainability Director, Infineum, Annie Jarquin, Director of Global Business Development, Kline Industries and Andréas Osbar, Vice President of Transformation Lubricants, Castrol will provide a platform for industry leaders to discuss the challenges the lubricant industry is facing and discuss the opportunities for agile stakeholders to harness this new normal for lubricants.

The next keynote session focuses on ‘Managing the Rapidly Changing Landscape in the Lubricant Value Chain’. Steve Holland, Former CEO, Brenntag will chair the session and Apu Gosalia, Sustainability Expert, Fokus Zukunft and Dr David Whitby, CEO, Pathmaster Marketing Ltd are teaming up in a lively session to explore what possible trends we can expect to see from the global markets in the coming months and years and how they might impact the lubricant industry, its end users and their combined push for a more sustainable future.

This free-to-attend event is a unique opportunity for customers, industry-leaders, pioneers and peers to share insights, innovation and lively debate about how to support end-users of lubricants in the most eco-friendly and economical manner. Attendees will come away from this event understanding the most pressing challenges and promising solutions for the whole supply chain; and will be able share their own insight with peers on how the industry can look to stimulate growth and development - profiting the sector, its customers, and the planet.

Paul Hooker, Event Director says “Lubricant Expo will feature a dedicated program of presentations and panel discussions, equipping attendees with the knowledge and supply-chain opportunities needed to achieve sustainability goals, reduce carbon, improve efficiency, and meet end-user requirements. This event is uniquely positioned to drive the conversation on what the industry could look like as we move through this decade. The exhibition and top-flight conference will connect the brightest R&D minds with the commercial voices needed to amplify and cement growth. From across the end user and manufacturing spectrum, leading speakers will address how to turn world-class R&D expertise into commercial opportunity and output.”

Lubricant Expo is co-located with the hugely anticipated The Bearing Show, Europe’s first dedicated free-to-attend, in person exhibition and conference – connecting bearing technology providers with the full range of end-user buyers, as well as the entire technology, equipment and materials supply chains.

For the full conference programme, exhibition enquiries and to stay up to date on all the latest news about Lubricant Expo please visit https://lubricantexpo.com/ and https://bearing-show.eu/

Hart makes assault on car battery market

Much is being debated about the electrification of transport with a particular focus on the  motorcar. This deliberation has accelerated thanks to increasing evidence of Climate Change with a growing focus on carbon emissions from vehicles.

The arrival of battery manufacturers to the British market such as Britishvolt, with its huge battery plant being built at Blyth, Northumberland, illustrates the level of change underway led by Nissan, at nearby Sunderland, where the manufacture of electric cars and as a consequence batteries started some 10 years ago. 

As Nick Hart, managing director, Hart Doors, Newcastle upon Tyne, explains. “We were asked to work with the design team at the initial design stages of the battery facility to manufacture a bespoke door system that would integrate with Nissan’s own systems. There are now some 100 Hart doors now in the battery part of the plant.

“We developed a unique door capable of giving 60-minute fire resistance and also be capable of completing up to 400,000 open/close cycles a year. Further, the doors met strict air leakage criteria and resistance to sudden air-pressure increases.

“The doors also interfaced with third-party equipment such as conveyor belt controls and fire alarms. Each had an LCD display control panel that provided a quick and easy diagnosis of what each door was doing at any point in time.

“Quite clearly this was a complex challenge for a new door system that had to perform in a demanding manufacturing environment and importantly comply with British, European and American standards,” says Mr Hart.

“The oven doors were by far the most sophisticated with each requiring a self-supporting fire rated frame. Every door required two  curtains, one that provided 60 minute fire resistance while the other one allowed the door to comply with the air leakage rates on the ovens.

“An additional benefit of the twin curtain design was the increased thermal performance of the door system as a result of the cavity created between the two door skins.”

Hart also supplied Cleanroom doors to control the environment which was an essential part of the  manufacturing process where environmental control was down to the smallest detail to ensure zero contamination.

Where fire protection was essential Hart fitted 60 minute fire screens at entry and exits points enabling them to close under a fire condition but also comply with the requirements of the Clean Room standard as well as being assessed against releasing fine particles in static and moving conditions.

Contact www.hartdoors.com  t: 0191 214 0404   This email address is being protected from spambots. You need JavaScript enabled to view it.

This website is owned and operated by: MSL Media Limited

msl logo
www.mslmedialtd.com

Co. Number: 05359182

© 2005 MSL Media Ltd. All rights reserved. E&OE

ems logo mobile