Fluke to showcase new cleantech tools and approaches for energy efficiency and safety at Light + Building

Visitors to ‘Light + Building’ can learn about Fluke’s range of testing and monitoring tools for building infrastructure and market-leading solutions for acoustic and thermal imaging, temperature measurement, calibration and condition monitoring at Stand B11 in Hall 12.

Eindhoven, Netherlands. 20 September 2022: Fluke, a global technology leader in the manufacture of compact, professional electronic test and measurement equipment, tools and software, will reveal a selection of new-to-market and rugged, handheld tools and approaches for energy efficiency, enhancing the adoption of cleantech technology and improving safety at this year’s Light + Building exhibition, held at Messe Frankfurt from October 2-6.

Light + Building is the world’s leading industry trade fair for lighting, design and intelligent building services technology solutions. During the five-day gathering of global industry leaders and stakeholders, Fluke will showcase its comprehensive range of sophisticated solutions across thermal and acoustic imaging, power quality and condition monitoring, and wiring system performance that enable installation professionals, electricians, civil engineers, and facility managers to safely detect and isolate faults.

Andreas Schuler, Electrical Sales Manager Germany at Fluke says: “Fluke is one of the leading global technology providers headquartered in Europe that specialises in helping small to medium sized businesses through to large blue-chip organisations to eliminate wasteful practices by becoming more energy efficient and safe. Fluke’s integrated solutions save customers time and money by combining industry-specific engineering with new technology to improve electrical and industrial installation, maintenance and service, precision measurement and quality control processes across many industries.” 

Fluke’s Stand B11 in Hall 12 will also be showcasing products from Beha-Amprobe, a leading provider of quality testing tools for electricians and HVAC technicians working in residential, industrial and commercial environments, located in Germany. The company was acquired by Fluke Corporation in 2003. 

Achieving energy efficiency

The company’s participation at Light + Building comes at a time of growing international and European initiatives to improve energy efficiency in buildings, which has a key role to play in achieving the European Green Deal’s ambitious goal of carbon-neutrality by 2050. Collectively, buildings are responsible for 40% of the European Union’s energy consumption and 36% of greenhouse gas emissions, which mainly stem from construction, usage, renovation, and demolition, according to the European Commission. HVAC systems alone account for 38% of a building’s energy consumption, equivalent to 12% of final energy usage.

Fluke’s dedicated solutions address the detection of the most common sources of energy loss and wastage found in commercial and residential buildings, including poor building insulation, leaks and wear in HVAC systems, as well as the operation and maintenance of electrical appliances and building systems. 

“Building and facility managers can struggle to accurately identify and isolate energy loss and measure efficiency improvements. However, Fluke’s easy-to-use tools for detection are designed to quickly and accurately identify faults so energy can be recovered and preserved for future use. In addition to this, our professional online tools and software solutions help companies to quantify the cost of leaks and other defects, prioritize them for repair and demonstrate return on investment,” said Mr Schuler.

“We are committed to improving the building, service and maintenance industries with our innovative product offering that aligns with European initiatives for sustainable infrastructure. We will continue to innovate and address the emerging needs of customers in response to the global shift towards sustainable development.”

Cleantech: Enhancing technology adoption

Cleantech technology relates to an approach to reduce the environmental impact of human activity through wasteful practices. Experts from Fluke will share their expertise and provide integrated solutions for renewable energy harvesting, electric vehicles and electric vehicle charging stations (EVCS).  

Fluke will be launching a new-to-market handheld tool used in the installation, commissioning, and routine maintenance testing of EVCS at Light + Building. The user-friendly tool is compatible with Fluke’s leading multifunction testers and can be paired with Fluke’s range of multimeters or scope meters for investigative troubleshooting.

“Testing of these high-power, live voltage electric systems is critical and must be completed every six to 12 months in accordance with strict international and European standards. The new safety features included in Fluke’s exciting new tool surpass other competitive products in the market,” commented Mr Schuler.  

Safety: trust the experts

Fluke helps companies overcome the skills gap in the workforce with its range of easy-to-use handheld tools and software, designed for the fast, safe and efficient detection of electrical system, networking and industrial equipment faults. 

As a leading provider of training programmes for installation and testing of electrical infrastructure in Germany and the United Kingdom, Fluke enforces safe workplaces through the provision of information about protective equipment, test tools and safety procedures based on Governmental and regional guidelines.

Fluke’s rugged handheld products have been rigorously tested to ensure safety in all forms of operation.

Get support

Fluke’s state-of-the-art range of testing and monitoring tools for building infrastructure, including electrical tools and network cable and appliance testers, as well as market-leading solutions for acoustic and thermal imaging, temperature measurement, calibration, and condition monitoring will be on display at Stand B11 in Hall 12 at Light + Building.   

FLUKE is a registered trademark of Fluke Corporation. For more information, visit the Fluke website at http://www.fluke.com.

WIPAC AND CONVERT CELEBRATE 15TH YEAR OF PARTNERSHIP AND OVER HALF A MILLION HARNESSES

Convert, the UK’s leading manufacturer of cable looms and harnesses, and Wipac are celebrating their 15th year of a partnership which has delivered over half a million harnesses for a wide range of high end cars.

The harnesses are for external lighting - head lights, rear lights including the centre high mount stop lights (CHMSL, the third brake lights) – and a range of printed circuit boards (PCB). In the past, lights were fairly straightforward to power, typically comprising two connecting wires, one carrying the earth, the other the current.

However, lights are now much more complicated as more functionality has been added, such as directional control of headlight beams, and the need to carry much more information. Modern cars can need up to 70 individual connections & terminations and up to 30 wires.

And with the introduction of communications and the flow of large amounts of data, they need to be able to withstand magnetic or electromagnetic interference. This is on top of different braiding to protect against extremes of temperature and ISO/TS standards to ensure chemical protection.

The PCBs have also brought a new level of complexity and handling, with connecting wires being as short as 20mm.

The partnership with Wipac, which designs and manufactures bespoke exterior lighting for the world’s leading performance and luxury automotive brands, has also benefitted Convert as a business, helping them to improve their own systems, with a continual focus on engineering excellence and customer service.

For example they designed a miniature, stand-alone waterproof grommet which forms an integral part of the cable harness for lamp enclosures.

The grommet uses tunnel guides to allow cable to pass through, creating a waterproof seal once fixed to the cable harness, which in turn remains stable and secure when fitted to a finished lamp.

The grommet meets waterproofing standard IP66K and is used in Wipac’s exterior lamps for British luxury and high performance sports car manufacturers.

Dave Lord, Convert’s managing director said: “Working with Wipac for the 15th year is a very different proposition from our early days, when all that was needed was the simplest of harnesses. Since then we have produced more complicated wiring sets for some of the biggest names in quality cars. And as we have grown, we have improved our systems and processes, with these best practice methodologies now standard across the board, driving improvement throughout the business.”

Georgina Westrope of Wipac added: “Convert is a fantastic example of a small UK company with excellence in electronics and engineering. Their technical know-how and customer service is second to none and we regularly involve the team in the design and development stages of our production.”

Convert supplies many advanced engineering industries, including automotive, public transport, medical and scientific equipment. It can produce all harness types, from multi-branch looms, interconnect harnesses and wire and cable sets, as well as more bespoke assemblies.

For more information, please visit https://www.convertltd.co.uk. 

200 and still counting!

15th September 2022, Dubai, UAE: We are delighted to be celebrating this, the 200th edition of The Maritime Standard newsletter. Packed with news and updates on the shipping and maritime sectors, the newsletter has been published without missing a single issue since its first one on June 1st, 2014.

It has proved to be extremely popular, steadily increasing circulation over this period, and moving from having a primarily regional to a genuinely global readership, indicating a strong demand for information and intelligence about developments in the Middle East and the Indian Subcontinent shipping, ports, and related sectors.

Clive Woodbridge, TMS Editor, says, “It is a fantastic achievement to be reaching this milestone and we are grateful for the support of our readers and sponsors over the past eight years. We have strived to cover what is important in the regional maritime sector and have tried to put an insightful spin on news about the industry, drawing on our years of experience. We have been fortunate to have a network of invaluable contacts at high levels throughout the sector who have been kind enough to grant us the benefit of their insights. Hopefully, as an increasingly global brand, we can continue to serve the market as a valuable source of information for the next 200 editions also.”

Over the past few years there have been a whole host of significant developments relating to the maritime sector in the Middle East and the Indian Subcontinent. Mergers and acquisitions; new port projects; investments in new ships; and upgrades to shipbuilding and repair facilities. The Maritime Standard has been there to cover them all, in a timely manner and with an easy-to-read format.

The pace of development and change will not slow down, and fresh and innovative ventures and business ideas will be coming to fruition. Once again, through The Maritime Standard, readers will not miss a thing.

Clive adds, “There is no doubt that the regional maritime business will grow and develop further over the next few years. It is a market that deserves close attention and about which up-to- date and insightful information can be important in identifying business opportunities and securing competitive advantage.”

The Maritime Standard is published by Flagship Events, a business which has been able to take full advantage of the wise leadership of the UAE, where it is based, to flourish as a media, events and conferences production company. The support given to the maritime sector by the leadership allowed activity to continue even during the pandemic, and this is truly appreciated.

The Maritime Standard also wishes to acknowledge the sponsorship and advertising support it has received from many of the region’s biggest companies. These include leading players in the ports, shipping, insurance, classification and marine services sectors.

TMS achievement in reaching the 200th edition has been praised by a number of prominent shipping and ports executives. Capt. Mohammed Juma Al Shamisi, Managing Director and Group CEO of Abu Dhabi Ports Group, commented “The progress that The Maritime Standard has made over the past eight years has been outstanding and we applaud the fact that it is now established as one of the leading online publications for the region.” Abdulla Bin Damithan, CEO & Managing Director DP World UAE & Jafza said, “The Maritime Standard provides us with an excellent, well written source of information and it has earned its position of respect across the industry.” Capt. Abdulkareem Al Masabi, CEO of ADNOC L&S, said. “The Maritime Standard newsletter has become an invaluable resource and it deserves every success. I wish it well for the future.” Dr Ibrahim Al Nadhairi CEO of ASYAD Shipping and Drydocks echoes these sentiments, saying: “The Maritime Standard has helped raise the profile of the maritime industries in this region and as such has made an extremely valuable contribution, which is widely appreciated and acknowledged.”

The TMS newsletter is the basis on which the TMS Awards and TMS Tanker Conference has taken root and flourished also. In November this year both events will return to the pre-covid venue of the Atlantis, one of the regions finest venues, and we are once again expecting a full house of over 800 people to pack the ballroom.

How to maximise energy efficiency in manufacturing

By Mark Bakker, Field Application Engineer, Fluke


Energy efficiency has always been a vital commodity in the manufacturing sector, but recent events have brought the discipline into much sharper focus. More than ever, today’s manufacturers cannot afford to waste a single joule if it can be avoided.

Of course, energy efficiency isn’t simply about minimising operational costs or protecting the environment. Other key benefits to manufacturers include being able to extend the working life of their expensive equipment while boosting productivity and performance levels.

Peak performance

In practice, energy efficiency relates to the ability to monitor whether machinery is operating at peak performance and identifies if motors and drives are being over- or under-loaded. This enables factory and plant managers to evaluate wastage in air compressors, process equipment and heating, ventilation, and air conditioning (HVAC) systems by monitoring and maximising power quality at every opportunity.

Equipment can be damaged or corroded in many ways that aren’t obvious to the human eye, resulting in wasted energy leaking away with nobody in the factory able to identify the source or how much wastage is occurring. Plant efficiency is so crucial that it can affect whether a manufacturer is able to meet the needs of customers, fulfil orders, retain staff and maintain competitive advantage in business. 

Electricity, water, gas and air

In manufacturing, the key areas where energy efficiency gains can be made are electricity, water, gas and air. The majority of downtime can be associated with these factors being poorly managed due damage or breakdowns in factory equipment and processes. Drilling down deeper, maintenance, repair and operations (MRO) engineers need to focus on battery efficiency, energy analysis and overall power quality as well as the fast and efficient identification of air, gas and vacuum leaks.  

Maintenance, Repair and Operations (MRO) engineers must rely on accurate logging equipment that is capable of recording and sharing real-time data on energy, load and power quality to optimise performance. Armed with this information, manufacturing companies can give themselves a clear picture of how healthy their electrical systems are. This enables teams to make informed decisions on what improvements need to be made in order to prevent costly equipment damage and achieve that elusive goal of maximising productivity and efficiency.

Power quality analysis

It is widely understood that poor power quality can lead to manufacturing equipment behaving unpredictably and even failing prematurely. If power quality is not checked regularly, problems can occur with motors, cables, transformers, capacitor banks and switch boards. Being able to test power quality as part of a routine maintenance programme will go a long way toward identifying potential and existing problems and dealing with them before they cause equipment failure and production line downtime.

Another issue is that power quality levels can be affected if a manufacturing facility installs new, complex machinery which alters plant dynamics. The more complex a manufacturing set-up becomes, the greater the likelihood that poor power quality will become a problem. To counter this complexity, it is essential to have a means of carrying out power quality analysis that is simple and safe. Ideally, the process shouldn’t take up significant time of critical personnel in the factory. Less experienced maintenance technicians should be able to perform inspections and draw up reports with ease.

Harmonics, dips and swells

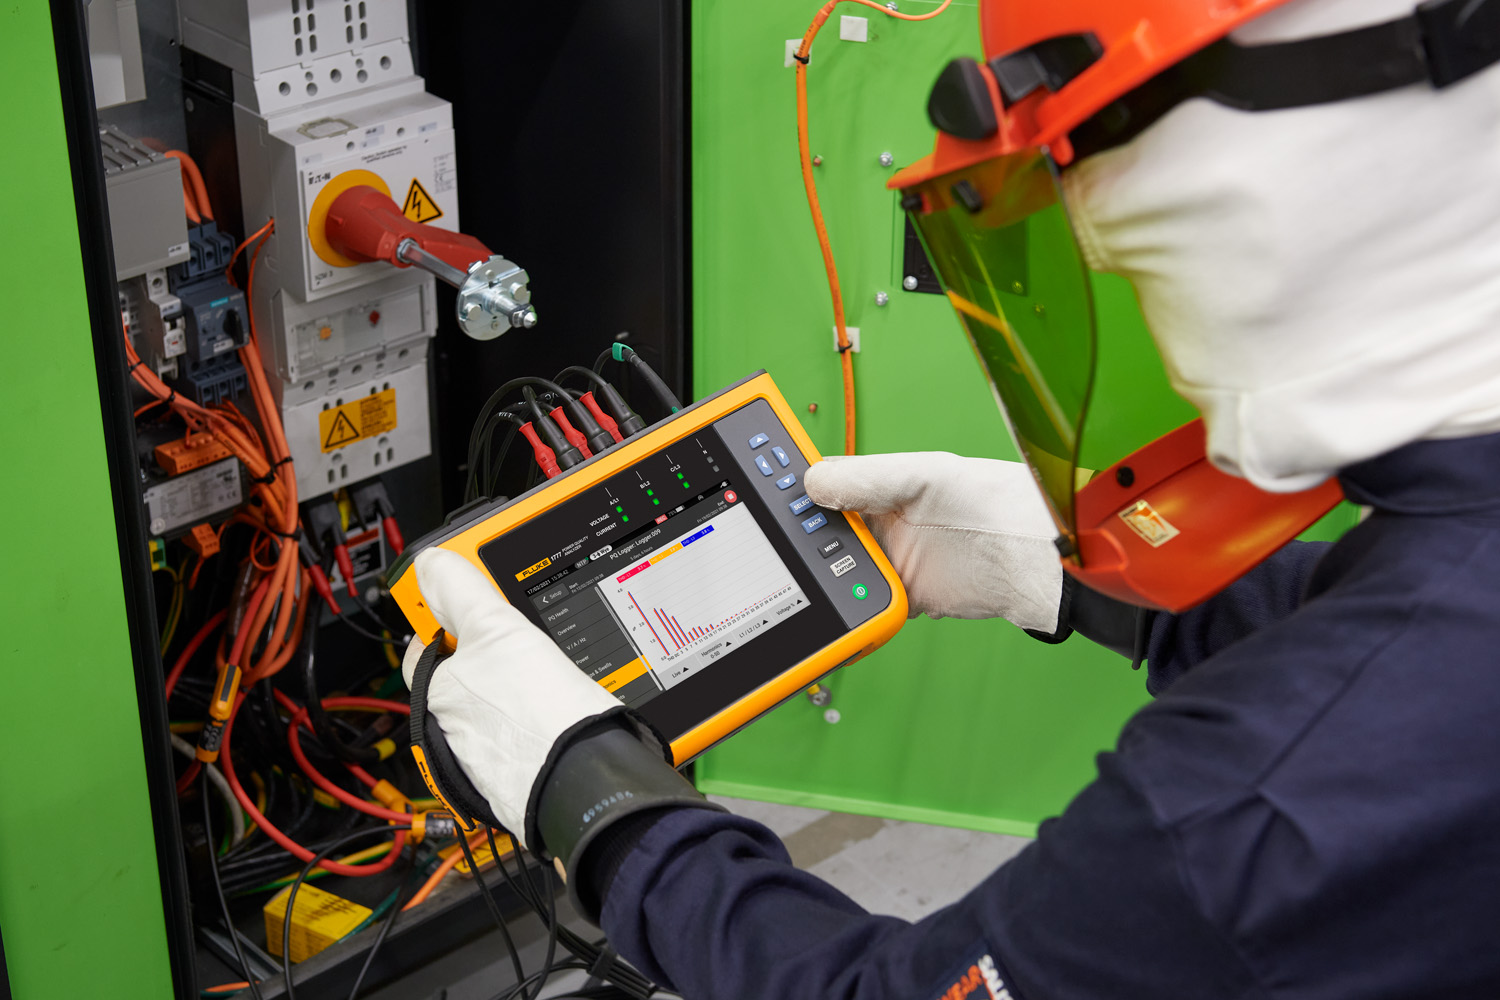
The Fluke 1770 Series Power Quality Analyser enables manufacturers to deliver productivity and efficiency gains. The tool is capable of automatically measuring and analysing power quality parameters such as voltage and current unbalance, transients, flicker, harmonics, dips and swells. By capturing high-speed voltage transients, the analyser enables engineers to mitigate their effects to prevent equipment failure. The data can then be shared immediately through Wi-Fi, the ethernet or a GSM network.

The beauty of the Fluke 1770 Series is that it combines in a single, hand-held unit the trouble-shooting capabilities of a power quality meter with the robust analysis and logging capabilities of a stand-alone power quality analyser. Also, with best-in-class specifications, the instrument can be powered directly from a measurement circuit, eliminating the need for a separate power outlet or extension cord.

Detecting air leaks

Air leaks are an issue in every manufacturing setting, but they are particularly problematic in the food and beverage (F&B) sector when it comes to managing energy efficiency. Even in today’s high-tech environments, maintenance engineers resort to listening for leaks or using the tried-and-tested soap and water technique. There are obvious drawbacks with these methods, not least the limited chance of hearing air hiss in a noisy factory, reaching piping in hazardous or difficult to access areas, and marking and recording the leaks for subsequent repair. 

A major soft drink bottling company in Germany had set itself tough new targets on the reduction of greenhouse gas (GHG) emissions and placed particular emphasis on cutting indirect emissions due to energy usage. More specifically, the company wanted to minimise the amount of energy that it was wasting because of undetected leaks in its compressed air systems. The production company estimated that using specific tools to quickly identify leaks had the potential to generate annual energy savings of up to €150,000.

Tests were conducted using Fluke’s ii900 Industrial Acoustic Imager. The tool’s array of 64 highly sensitive microphones showed that it was possible for maintenance engineers with little experience to obtain accurate, real-time data on air, gas and vacuum leaks in the factory’s compressed air systems. The data was shown on an easy-to-read LCD display.

Today, the global F&B company is using the point-and-shoot acoustic imager to identify compressed air leaks in hard-to-reach gated areas, overhead piping systems and in tubing, hoses, fittings and valves flanges and valves in the CO2 blender, syrup maker and ‘clean-in-place’ system. No longer do engineers need to scale ladders and take photographs to pass this information onto colleagues. In addition to this, the plant has eliminated the need for unplanned shutdowns while the leak detection process is underway. The team can also rank leaks in order of seriousness to produce a prioritised maintenance schedule, and once repairs have been made engineers can use the Fluke ii900 Industrial Acoustic Imager to check them.

The bottling plant energy manager commented: “This innovative technology was purchased for localising leaks in our compressed air systems throughout the plant. We have already seen enormous energy savings.”

Recovered capacity

In another example using the same acoustic imaging equipment, a USA-based global manufacturer of aerial lift equipment set a goal to become more energy efficient by detecting and repairing leaks. Genie (a Terex brand) estimated that it used between 1,800CFM and 2,600CFM of compressed air every day to operate up to 200 torque tools per line as well as equipment that moved large sheets of half inch steel. If the compressed air pressure was compromised in any way, the result could be the loss of up to 200,000 parts.

Some leaks were found in the hoses located high up in the factory’s rafters. Checking the hoses and locating the individual leaks in the system was difficult and time consuming. Finding a single leak could take up to 45 minutes, according to maintenance supervisor Josh Stockert. He confirmed that acoustic imaging had resulted in the factory recovering 25.7% of compressed air capacity which represents annual energy savings of USD $48,754. The savings were accurately recorded by a Fluke 3540 FC Three-Phase Power Monitor.

“We were near the top end of what our compressor system can put out,” Stockert said. “By correcting the leaks found using the ii900, one of our four compressors is nearly idle much of the time.”

He added: “It takes me all of 30 seconds to a minute to find an air leak with the ii900. Some days we can find and repair 30 or 40 leaks in just a couple hours. Plus, we can use the ii900 during production hours, when it’s extremely loud, and still been able to capture leaks at the rafter level up to six to 9 meters (20 to 30 feet) away.”

Multi-function calibrations

Manufacturers looking to maximise energy efficiency also understand the need to carry out regular inspection, testing and calibration on the vast number of process control equipment that operate in their factories. The performance of electronic instruments can change over time due to exposure of the electronics and the primary sensing element to varying temperatures and humidity, as well as pollutants and vibration. One problem with checking such equipment is that it often needs to work continuously and at peak levels of reliably and accuracy, which means it isn’t feasible to stop production operations to carry out the calibration process.

Many companies have turned to multi-function calibrators which enable sensors and transmitters and other essential equipment around the plant to be checked in-situ and without the need for a highly skilled calibration technician to be on-site. The Fluke 754 Documenting Process Calibrator with HART communication solves this problem by performing the functions of several tools. It can source, simulate and measure pressure, temperature and electrical signals in a single hand-held device. The unit also automates calibration procedures and captures data, eliminating the practice of documenting calibration records by hand which is still used in many factories today.  

With a robust range of tools available, the ability to maximise energy efficiency across many critical areas in manufacturing has been given a substantial boost to the sector, enabling businesses to achieve their sustainability goals.

TIDAL TURBINE TO LIGHT THE THAMES

A small proportion of the Thames is to be illuminated using power generated by the flow of the river itself, as Kingston University tests prototypes of a new hydroelectric turbine design.

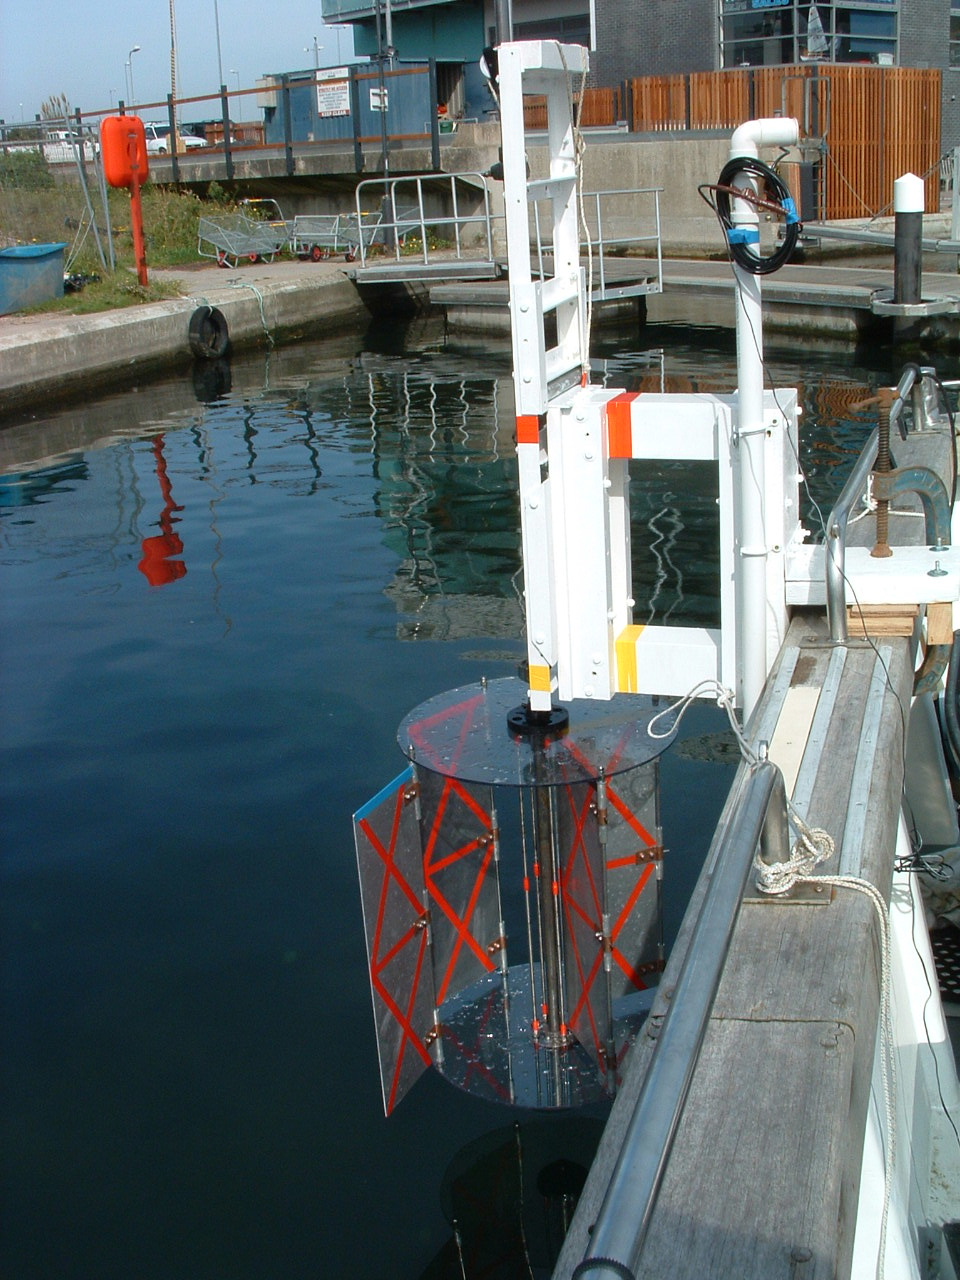
The turbine will sit on a pontoon and will provide a floating test and measurement laboratory. On this will be an array of sensors and monitors, including a TorqSense the wireless torque sensor from Sensor Technology Ltd.

"To say that this is a harsh environment for laboratory equipment is a bit of an
understatement," says Rod Bromfield, Senior Lecturer, of the Faculty of Engineering, Kingston University.  "We can only use robust kit with a proven industrial pedigree."

The turbine under test has been developed by Hales Marine Energy near Eastbourne on the English south coast and is expected to be deployable in tidal seas as well as rivers. The design application of this turbine is to sit on a submergible tank that will sit on the sea bed and can be floated up to the surface when required. Significantly, the design is almost infinitely scalable: the unit under test is 1m diameter and produces about 1kW; 5m turbines suitable for inshore deployment would generate round 20kW; smaller units would be ideal for river use. With access to the test site being by small boat, Rod knew that his test regime had to be both simple and comprehensive.

"The critical measurement is torque, as this indicates the power we can derive from the system. We had to be certain that we would get continuous measurements over an extended period of time, because we need to map power production against actual river flow. Also for this technology to succeed in the emerging green power market it must be capable of continuous and predictable energy production."
One of the engineering issues that Rod faced was the relatively slow revolution of the turbine, in this test below 50rpm. This helped define the choice of the TorqSense, but it is also a key feature of the Hales turbine - the slow speed means less stress on moving parts and therefore less servicing. It also minimises habitat disturbance, so that the ecological impact is low.


"When I contacted Sensor Technology I was very concerned about vertical mounting and harsh environment performance," recalls Rod. "Fortunately there have been TorqSenses installed vertically, including several high up on vertical axis wind turbines, where they have to withstand gales, hurricanes and lashing rain."

Turbine
The design of the Hales turbine is reassuringly simple, and therefore likely to survive underwater installation with long service intervals. It was developed by Paul Hales, a design engineer who has spent a career associated with the sea.  "It’s based on the traditional water wheel, but mounted on a vertical axis - on its side," he explains.
"Using modern engineering and materials it is possible to take this effective early turbine and by turning the output shaft to the vertical to immerse the whole turbine into the tidal flow. To overcome the high resistance on the wheel blades that on one side are trying to move against the water flow, they are shaped and hinged to present a minimum resistance. The large blade area on the drive side produces very high amounts of torque (rotational force) at low speed, in the range of 10 -20rpm.

Coupled with modern permanent magnet generators that can start producing electricity rotations as low as 2rpm, my turbine can offer the possibility of tidal generation worldwide.”

Paul continues: "Water is nearly 800 times denser than air so it carries far more energy, making water turbines a very attractive alternative to wind energy. Notably seabed systems are not an impediment to shipping, nor do they have any visual impact and ecological issues are minimal for low speed systems."

Paul says that he could envision an array of his turbines on every headland along the English Channel and at intervals down the Thames.

"Of course, that is just the start. The simplicity of the design, its robustness and low maintenance, relative ease of installation all add up to making it suitable for deployment in remote and less developed areas. Its low ecological footprint addresses many of the issues raised by environmentalists. Its continuous and utterly predictable power output overcomes the intermittency associated with wind, wave and solar power.


"When, over the test period, people stand on Richmond Bridge and watch a modest array of lights bobbing about on a buoy, they may not know it but they will be seeing the future!" 

Morris Lubricants new video series helps customers understand how oil is made

A new video series has been release by Morris Lubricants - designed to provide end users and distributors across a variety of market sectors with an insight into how oil is made and the factors that should be considered when choosing a lubricant supplier.

The series of five short videos demonstrates the key areas that should be considered when selecting oils and lubricants, to ensure maximum equipment life and reduced production downtime.

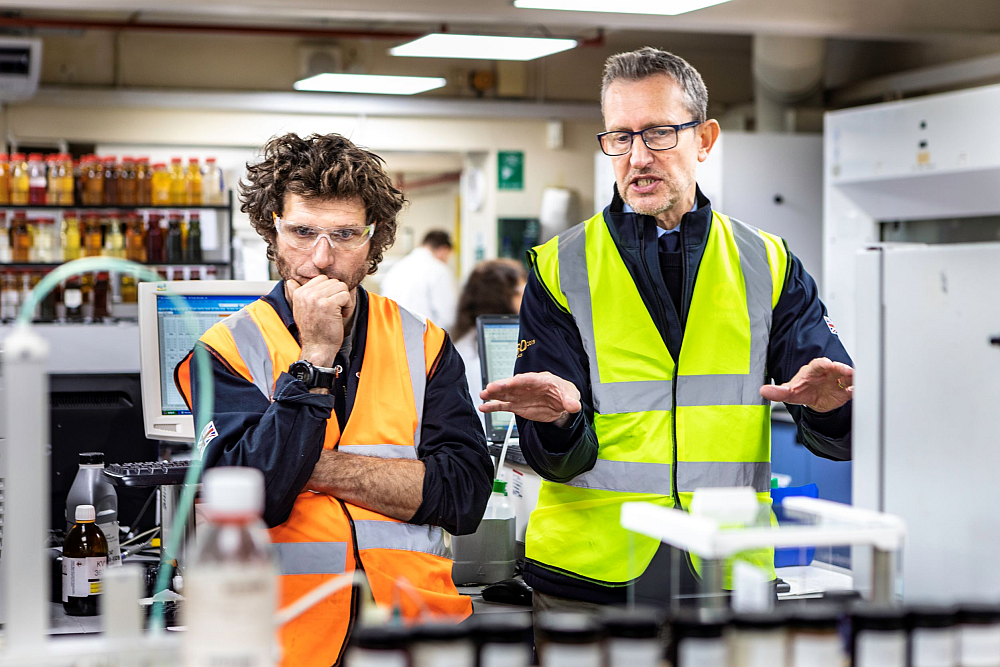
The videos feature Guy Martin, lorry mechanic, motorbike racer, TV presenter, engineering enthusiast and Morris Lubricants’ ambassador who is taken through the production process. A heavy goods vehicle mechanic by trade, Guy was eager to discover each stage of the manufacturing process and how oil is formulated to keep mechanical systems lubricated even in the toughest conditions.

The video explains that the oil blending process is strictly monitored, beginning with the raw materials, which includes base oils and additive chemistry being delivered into the Shrewsbury manufacturing facility.

A stringent quality assurance process is then followed. All the base oil and additives delivered to the company are quarantined, sampled and sent to the on-site quality control (QC) laboratory where they are subjected to a suite of tests to ensure they are suitable for use. The Morris Lubricants’ QC laboratory currently conducts more than 5,000 quality control tests a month.

Once approved, these materials are released for production and are then carefully blended together, in compliance with strict formulation guidelines, to produce the finished high quality lubricant.

Each oil product is specially formulated to meet the needs of individual applications alongside strict global and original equipment manufacturers’ (OEM) specifications.

The blended lubricant is then sampled, sent to the QC laboratory and subjected to a series of chemical and physical tests. This ensures the formulation has been followed exactly.

When approved by the QC laboratory, the sample is released for filling. Once again, before filling begins, a final sample is taken from the filling head and checked a final time to ensure compliance.  

The approved lubricant can then be filled into the appropriately labelled and batch numbered package. The pack sizes filled with lubricant ranges from 1 litre bottles, 5 litre contours and 25 litre drums to 205 litre barrels as well as bulk containers. This process ensures full traceability of the quality of the finished product.

The finished product is palletised, stored and then shipped out to customers in the UK or overseas. 44 million litres of product leave the company’s two manufacturing sites per annum, with 12 shipping containers leaving Shrewsbury every week to supply quality products to customers all around the world.

About the episodes

The video series starts with Episode one and highlights the arrival of various high quality raw materials coming from the numerous suppliers based all around the world.

Episode two covers the processes that are conducted in the QC laboratory which conducts more than 5,000 tests a month.

Episode three explains the computer-controlled blending process and an eco-friendly ultrasonic technique which has cut blending time from 60 to 10 minutes. The company has the versatility to blend volumes from 200 to 70,000 litres.

Episode four takes viewers to the filling lines where various packaging formats are available to satisfy a diverse range of customers.

Episode five focuses on storing and shipping products which each have tamper-proof seals. The company ships oil and lubricants around the globe with 12 containers leaving Shrewsbury every week.


“After spending time at the factory in Shrewsbury, I now appreciate the science and skill that goes into the oil production process,” said Guy. “I didn't realise the company produced so many different varieties of oil and lubricants.

“It blew my mind when Adrian said that Morris Lubricants ships 12 containers of oil a week to countries as far away as New Zealand, Iraq and China and how much trust their international customers have in the product being made in Britain.”

Adrian added: “Guy was genuinely interested in the process, spontaneous with his comments and amazed by what goes on behind the scenes,” he said.

“He was excited by the prospect of trying something new and enjoyed filling a few barrels, capping them and putting the Morris Lubricants seals in place.

The video series has been launched on Morris Lubricants website and Facebook and can be viewed at

Fluke Networks invites customers to save up to £4,000 on selected copper and fibre testers

In recognition of Fluke Networks 30th anniversary, customers can now benefit from a limited time discount offer on many of the bestselling copper and fibre solutions designed for installing and testing critical networking infrastructure.


Eindhoven, Netherlands. 6 September 2022: Fluke Networks, a worldwide leader in certification, troubleshooting and installation tools for professionals who install and maintain critical network cabling infrastructure, has today announced a new limited time discount promotion on a range of bestselling copper and fibre testing solutions, with savings of up to £4,000.

The ‘No fuss. Just savings’ offer was developed in celebration of Fluke Network’s 30-year anniversary, following the launch of the company’s first cable tester in December 1992. Customers are invited to take advantage of exclusive savings on a wide range of products, with discounts of £800 offered on the DSX-602 PRO CableAnalyser through to £4,000 on the DSX2-5000QI-G-INT CableAnalyser.

The substantial discounts are available to all customers in Europe, the Middle East, Africa and the Commonwealth of Independent states (EMEACIS). The offer is available for a limited time between September and December 2022 and is valid with purchases of qualifying products only made from Fluke Network’s authorised distributors.

Robert Luijten, Fluke’s Training Manager and Test & Measurement Expert said: “We are pleased to provide our customers with a limited-time discount on some of the most powerful and sophisticated copper and fiber testing solutions available in the market. Historically, Fluke Networks has provided loyal customers with great opportunities to move up to the next generation of testers with our popular trade-in programmes. Many customers have taken advantage of this over the years. However, our new ‘No fuss. Just savings’ offer no longer requires trade-ins. Customers can now enjoy no returns, registrations, or hassles – all they must do is contact their local distributor to take advantage of these great discounts.”

Resolve and prevent network connectivity faults

Fluke Networks range of testers for twisted pair copper cabling can locate connectivity faults quickly to minimise downtime and lost productivity. The testers provide accurate, error-free certification even in the most complex projects that may involve several teams, different media types and multiple testing requirements. The range can be used to test up to Cat.8 cabling that can support the transmission of data up to 40Gbps over balanced twisted-pair copper cabling.

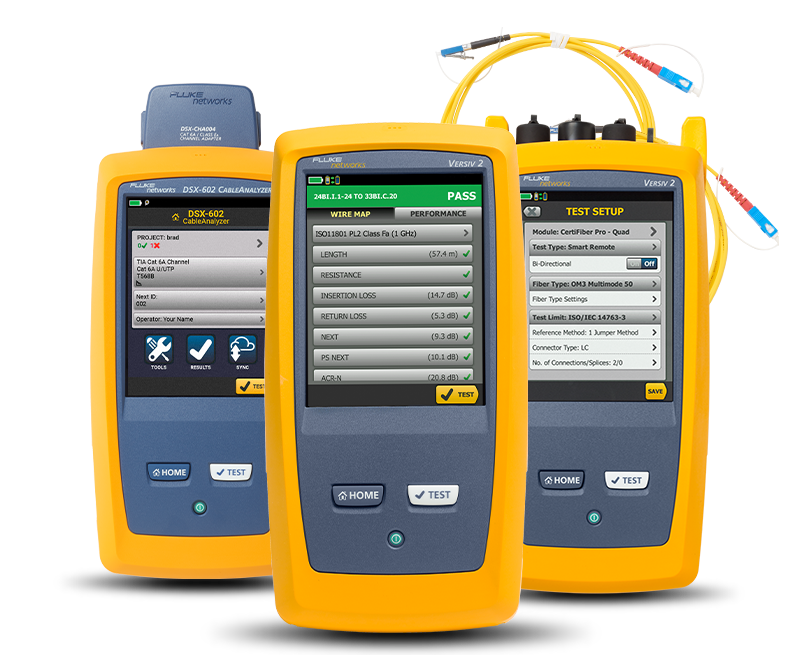
The DSX is built on Fluke Networks’ modular Versiv™ cabling certification system that can cut cabling installation and maintenance costs by up to 65%. Cornerstones of the Versiv system are the intuitive Taptive™ Graphical User Interface for ease of use and error-free operation and the ProjX™ management system which ensure that all testing is carried out efficiently and correctly. The Versiv system was recently upgraded with a high dynamic range Optical Time Domain Reflectometer (OTDR) and an MPO fibre inspection camera.

Accelerate fibre testing and certification

Fluke Networks’ fibre testing tools are the preferred option for network cabling installers, architects, technicians, and engineers due to their rugged design, accuracy and ease of use. While fibre optics has become the preferred option for reliable connectivity within smart buildings, data centres and other networked environments, locating faults can be a lengthy and costly process. The Versiv-based OptiFiber Pro OTDR makes this easy. Thanks to the EventMap function, the tool automatically identifies events including connectors, splices, bends and splitters.

The CertiFiber Pro, another feature of Fluke Networks’ Versiv system, offers an optical loss test set with the fastest time to certify. This means two fibres at two wavelengths can be measured in just under three seconds, providing automatic pass/fail analysis to meet critical industry standards or custom test limits.

Depending on the modules that are inserted in the Versiv mainframes, the system transforms itself into a copper cable tester (DSX), fiber loss and length tester (CertiFiber Pro), an OTDR (OptiFiber Pro) or into a fiber inspection instrument with a camera (Fiber Inspector Pro or Fiber Inspector Ultra). All products feature the same user-friendly interface. Being able to operate and program different testers with a common user interface is unique in the industry. Moreover, the measurement data gathered by the different testers can be easily consolidated in a single report by a LinkWare-supported personal computer or a LinkWare Live cloud-based service. LinkWare Live enables Project Managers to manage jobs and testers from any smart device.

For more information about the ‘No Fuss. Just savings’ campaign by Fluke Networks, go to: www.flukenetworks.com/nfjspromoUK.

New MD, expansion and sales growth outline bright future for Hi-line

Hi-line Industries, a UK-based leader in the design, manufacture and installation of energy-efficient compressed air purification equipment, has appointed Steve Smith as its new Managing Director. Replacing Mike Thurlow, who has retired, Smith is part of the company’s original team, joining as Marketing Director in 2000 when the business began trading. He has purchased Thurlow’s 50% share of the business and is now busy making plans to drive even greater success at Hi-line.

The outlook is extremely positive for this innovative and progressive UK manufacturer. At year-end (31 July 2022), Hi-line showed 27% growth in like-for-like sales, underpinned by a record year for the company’s N2 nitrogen generator systems and HPSA desiccant dryers, both of which have features and functions that provide notable market differentiation. 

Keeping pace with growing order levels is driving expansion at Hi-line’s Burton-upon-Trent headquarters and production facility. A new building extension is under design, but such is current demand that the company recently erected two temporary warehouse buildings simply to hold the additional materials required for dryer builds. Several six-figure projects are underway for completion before year-end.

                                                                                                                                                                        Continued ……

“This company has come a long when since it began in 2000, but we can achieve even more,” says Smith. “We have new teams in the warehouse and service departments, which will help support our future growth in terms of both physical size and revenue. Despite our ambitions, however, the company’s founding principles will not change. Our experienced and qualified engineers will continue designing and building to the highest standards. We have great confidence in our high-quality workmanship and materials, which reflects in our five-year warranty. I’m very excited to spearhead our ongoing development in the coming years.”

Hi-line is ISO9001 certified and a member of the British Compressed Air Society. The company also supports the ‘Made in Britain’ campaign, which highlights the passion around British-made brands and UK manufacturing. Hi-line’s broad range of energy-efficient compressed air equipment includes air dryers, nitrogen and oxygen generators, filtration equipment, condensate management/drains, and service kits.

www.hilineindustries.com

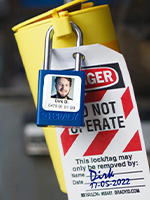
Smart way to make machine interventions safer

LOTO-Personalised-150x200.jpg          


Increase workplace safety with a world-class Lockout/Tagout solution from a single supplier.


Easily de-energise machines during maintenance to prevent accidents related to moving machine parts and any type of machine energy. Manufacturers worldwide use solution from Brady Corporation to optimise existing, and to implement complete Lockout/Tagout programmes that maximise workplace safety and protect employees. There are 7 reasons Brady is the preferred partner in Lockout/Tagout projects. Check them out!


A complete Lockout/Tagout implementation from A to Z:


  • Best-in-class lockout procedures:
    • no time to set up safe Lockout/Tagout procedures? Invite a Brady Safety Engineer to identify all machine energy isolation points and create illustrated, machine specific, world-wide best practice Lockout/Tagout procedures for your approval.
  • Optimal procedure management:
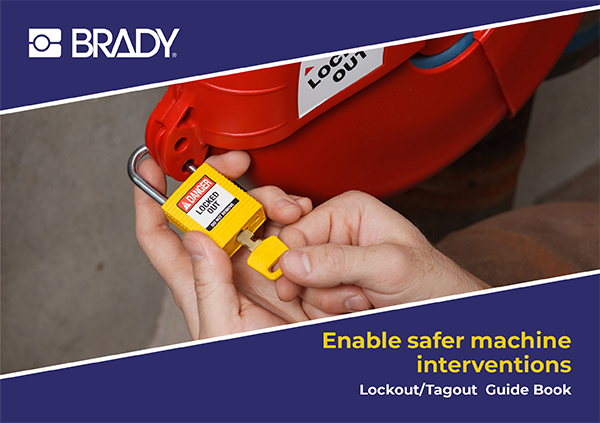
    • LoToGuideBookCover-EN.pngthe process of managing, creating, updating, reviewing, scaling and communicating visually instructive lockout procedures becomes a matter of clicks.
  • Block access to any energy control point:
    • temporarily block access to valves, buttons, fuses and any energy isolation point with our complete range of dedicated Lockout/Tagout devices.
  • Best safety padlocks in the world:
    • effectively secure the isolated state of your machines during maintenance with our unique SafeKey padlocks that offer 700% more lock and key options for elaborate, futureproof lockout programmes.
  • Reliably identify every lockout:
    • easily communicate about ongoing maintenance interventions with reliable Lockout/Tagout tags that can be delivered to, or created at your premises with our safety printers.
  • Practical lockouts:
    • make Lockout/Tagout even more practical and efficient using our wide range of clever accessories.
  • Easily distribute lockout tools:
    • highlight the right solutions for specific lockouts, and encourage tool returns to the right location with our custom shadow boards.

Discover complete Lockout/Tagout solution from Brady and download the free guide “Enable Safer Machine Intervention” >>

Brady Corporation

www.brady.co.uk

Remove rust easily without harming the environment

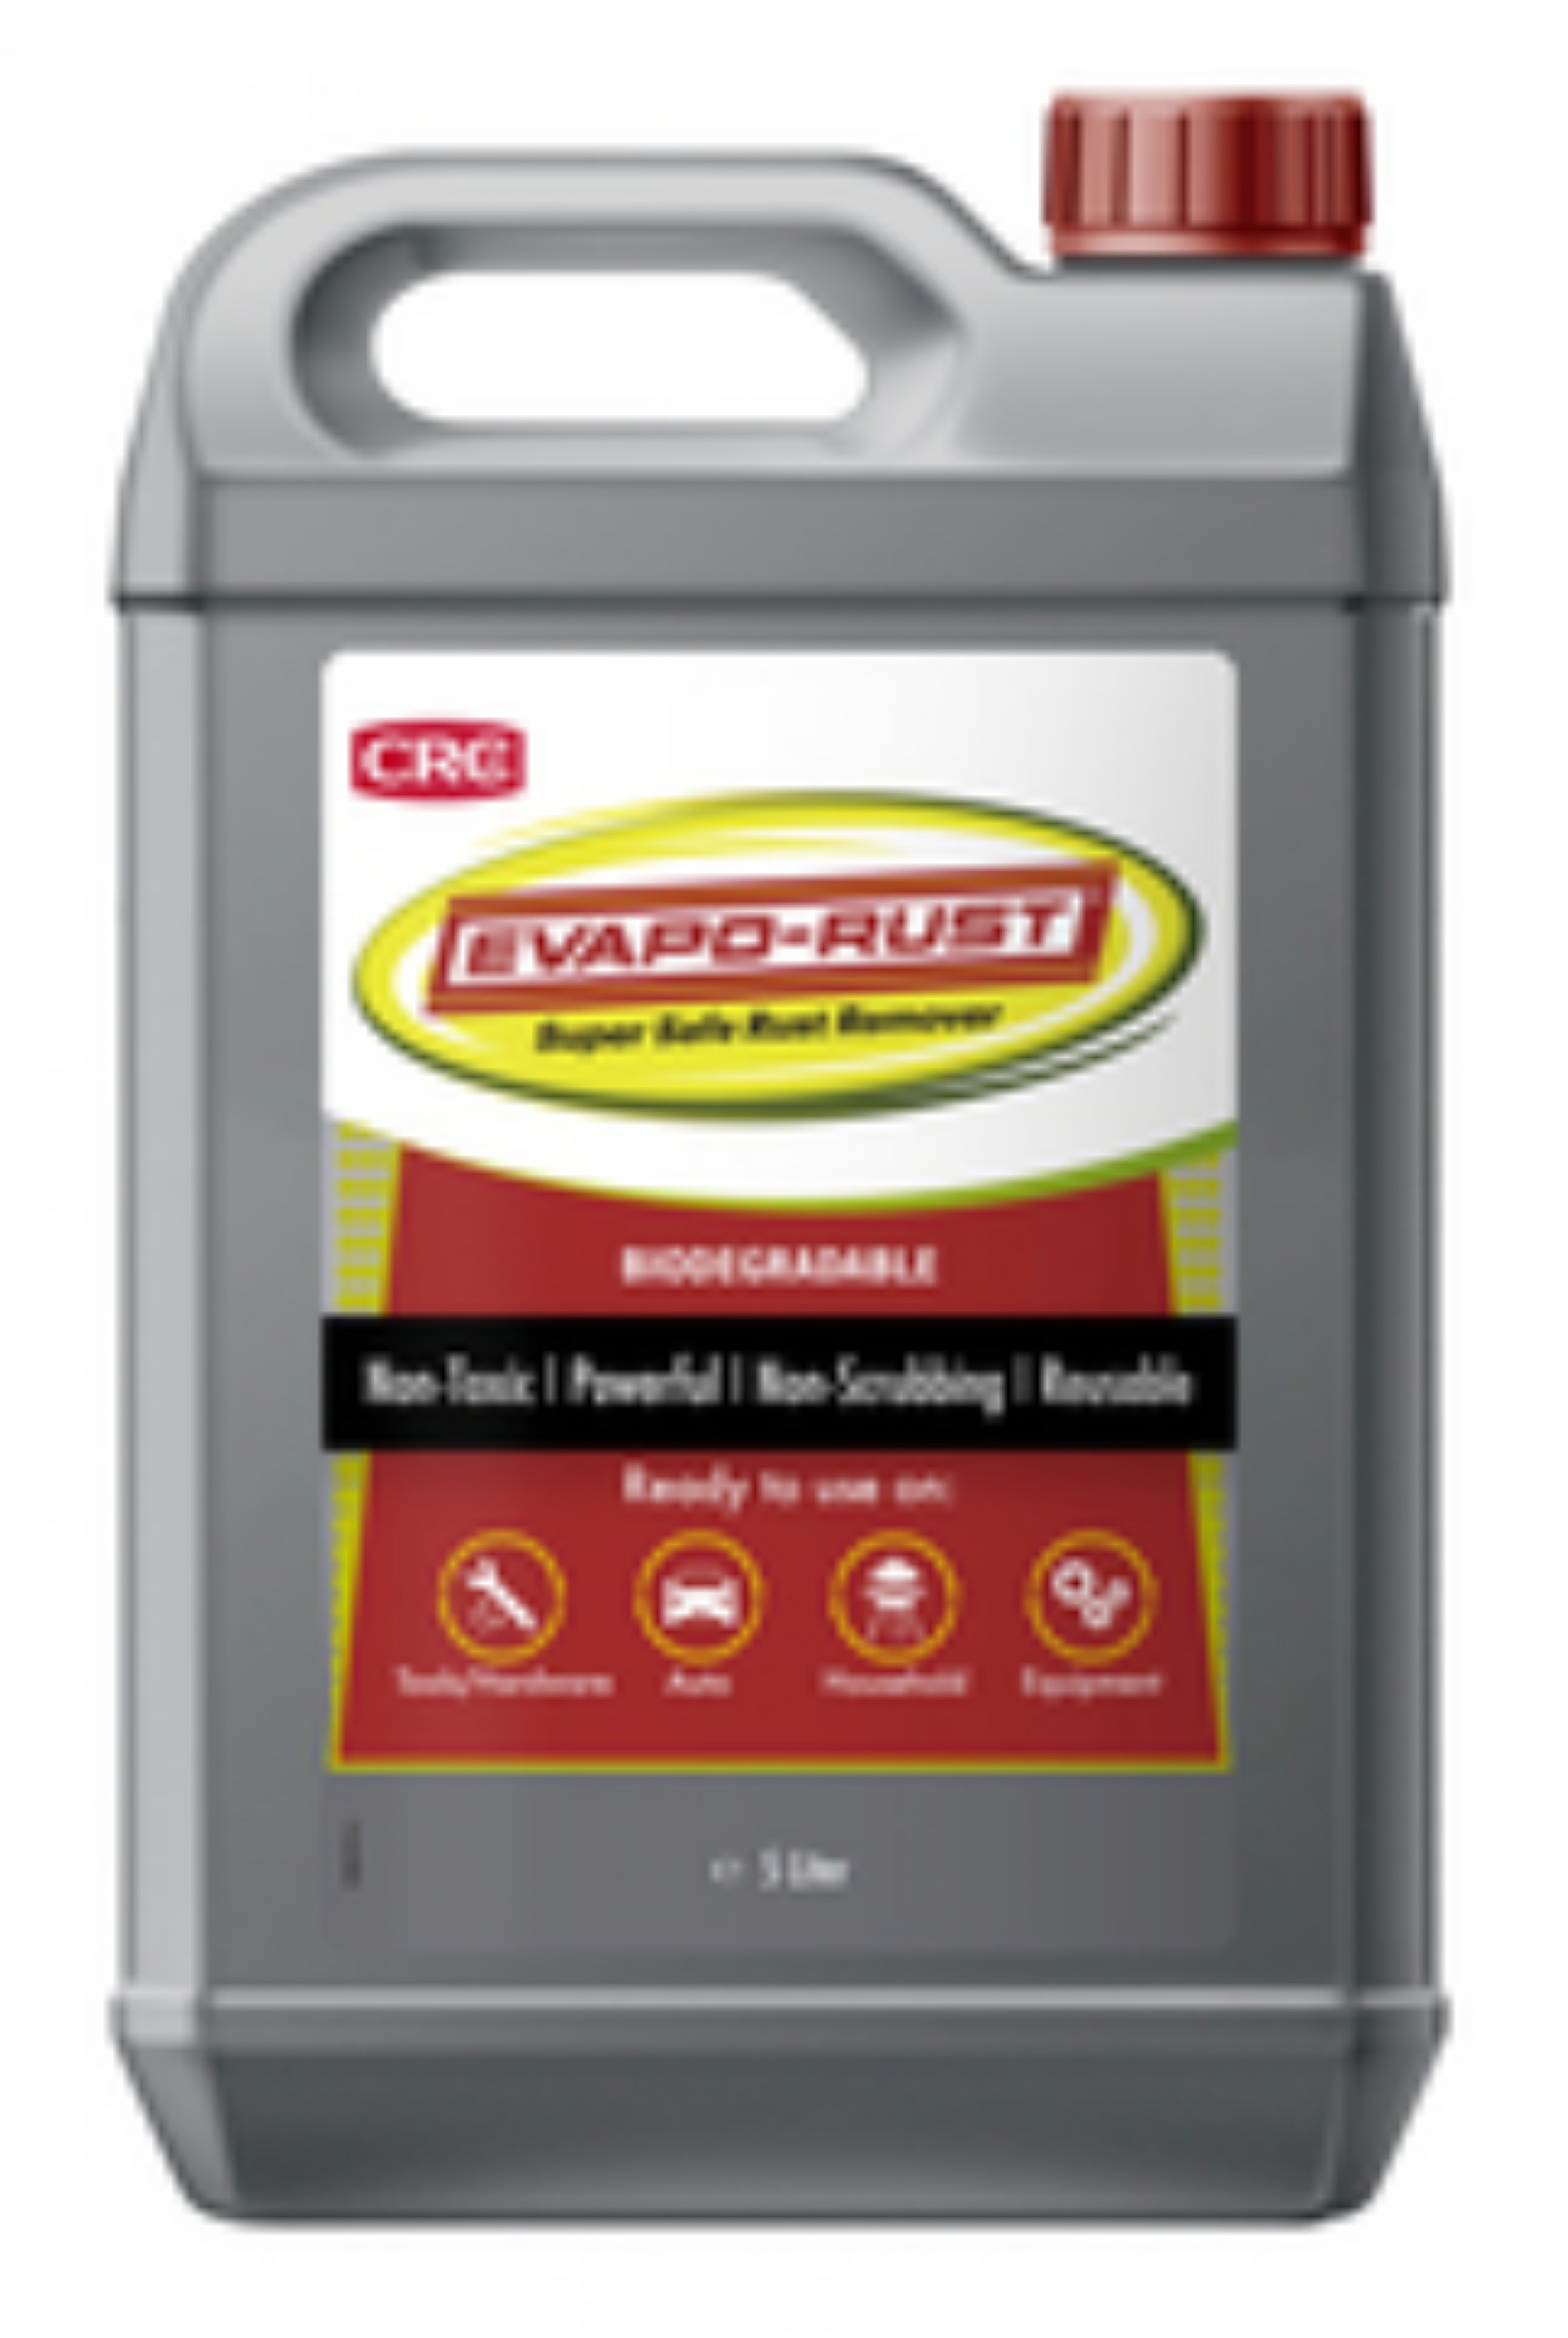
Evapo-Rust from CRC Industries is a water-based rust remover that is biodegradable and non-toxic for the user and the environment. Its formula eliminates rust without having to scrub or sand the parts being treated. The part simply has to be immersed in a bath of the ready-to-use solution, the rust then detaches from the metal surface and remains suspended in the liquid. Compared to conventional acidic or basic strippers, CRC Evapo-Rust is non-toxic, non-caustic and non-corrosive, and does not affect plastic, PVC, Viton and non-oxidized paint on treated parts.

The treatment is fast, a light layer of rust is removed in only 15 to 30 minutes, a medium layer in 6 hours, and a thick layer in 12 to 24 hours.

Several reuse cycles

The same CRC Evapo-Rust bath can be reused several times, depending on the intensity of the rust layer on the treated parts, which makes it economical. 5 litres of Evapo-Rust can remove 0.3 Kg of pure dry rust. Moreover, preliminary cleaning is only necessary in the case of very dirty and greasy parts. Once the part has been derusted, you only need to rinse it with water.

The reausable Evapo-Rust can be used to restore metal parts and tools rapidly and efficiently in all types of industry: automotive, construction, marine, metalworking, etc.

Safe to use for both the user and the environment

CRC Evapo-Rust's water-based formula, readily biodegradable in accordance with the OECD 301B standard, does not emit any unpleasant odours or volatile organic compounds (VOC) that could potentially harm the environment. It is perfectly soluble in water and is easily removed after use. It is ph-neutral, so it presents no risk of skin irritation or danger to the user´s eyes. Moreover, it is non-flammable, which simplifies its conditions of use and storage.

CRC Evapo-Rust is available in 1l, 5l and 20l drums, with labelling in 24 languages. It is REACH compliant.  

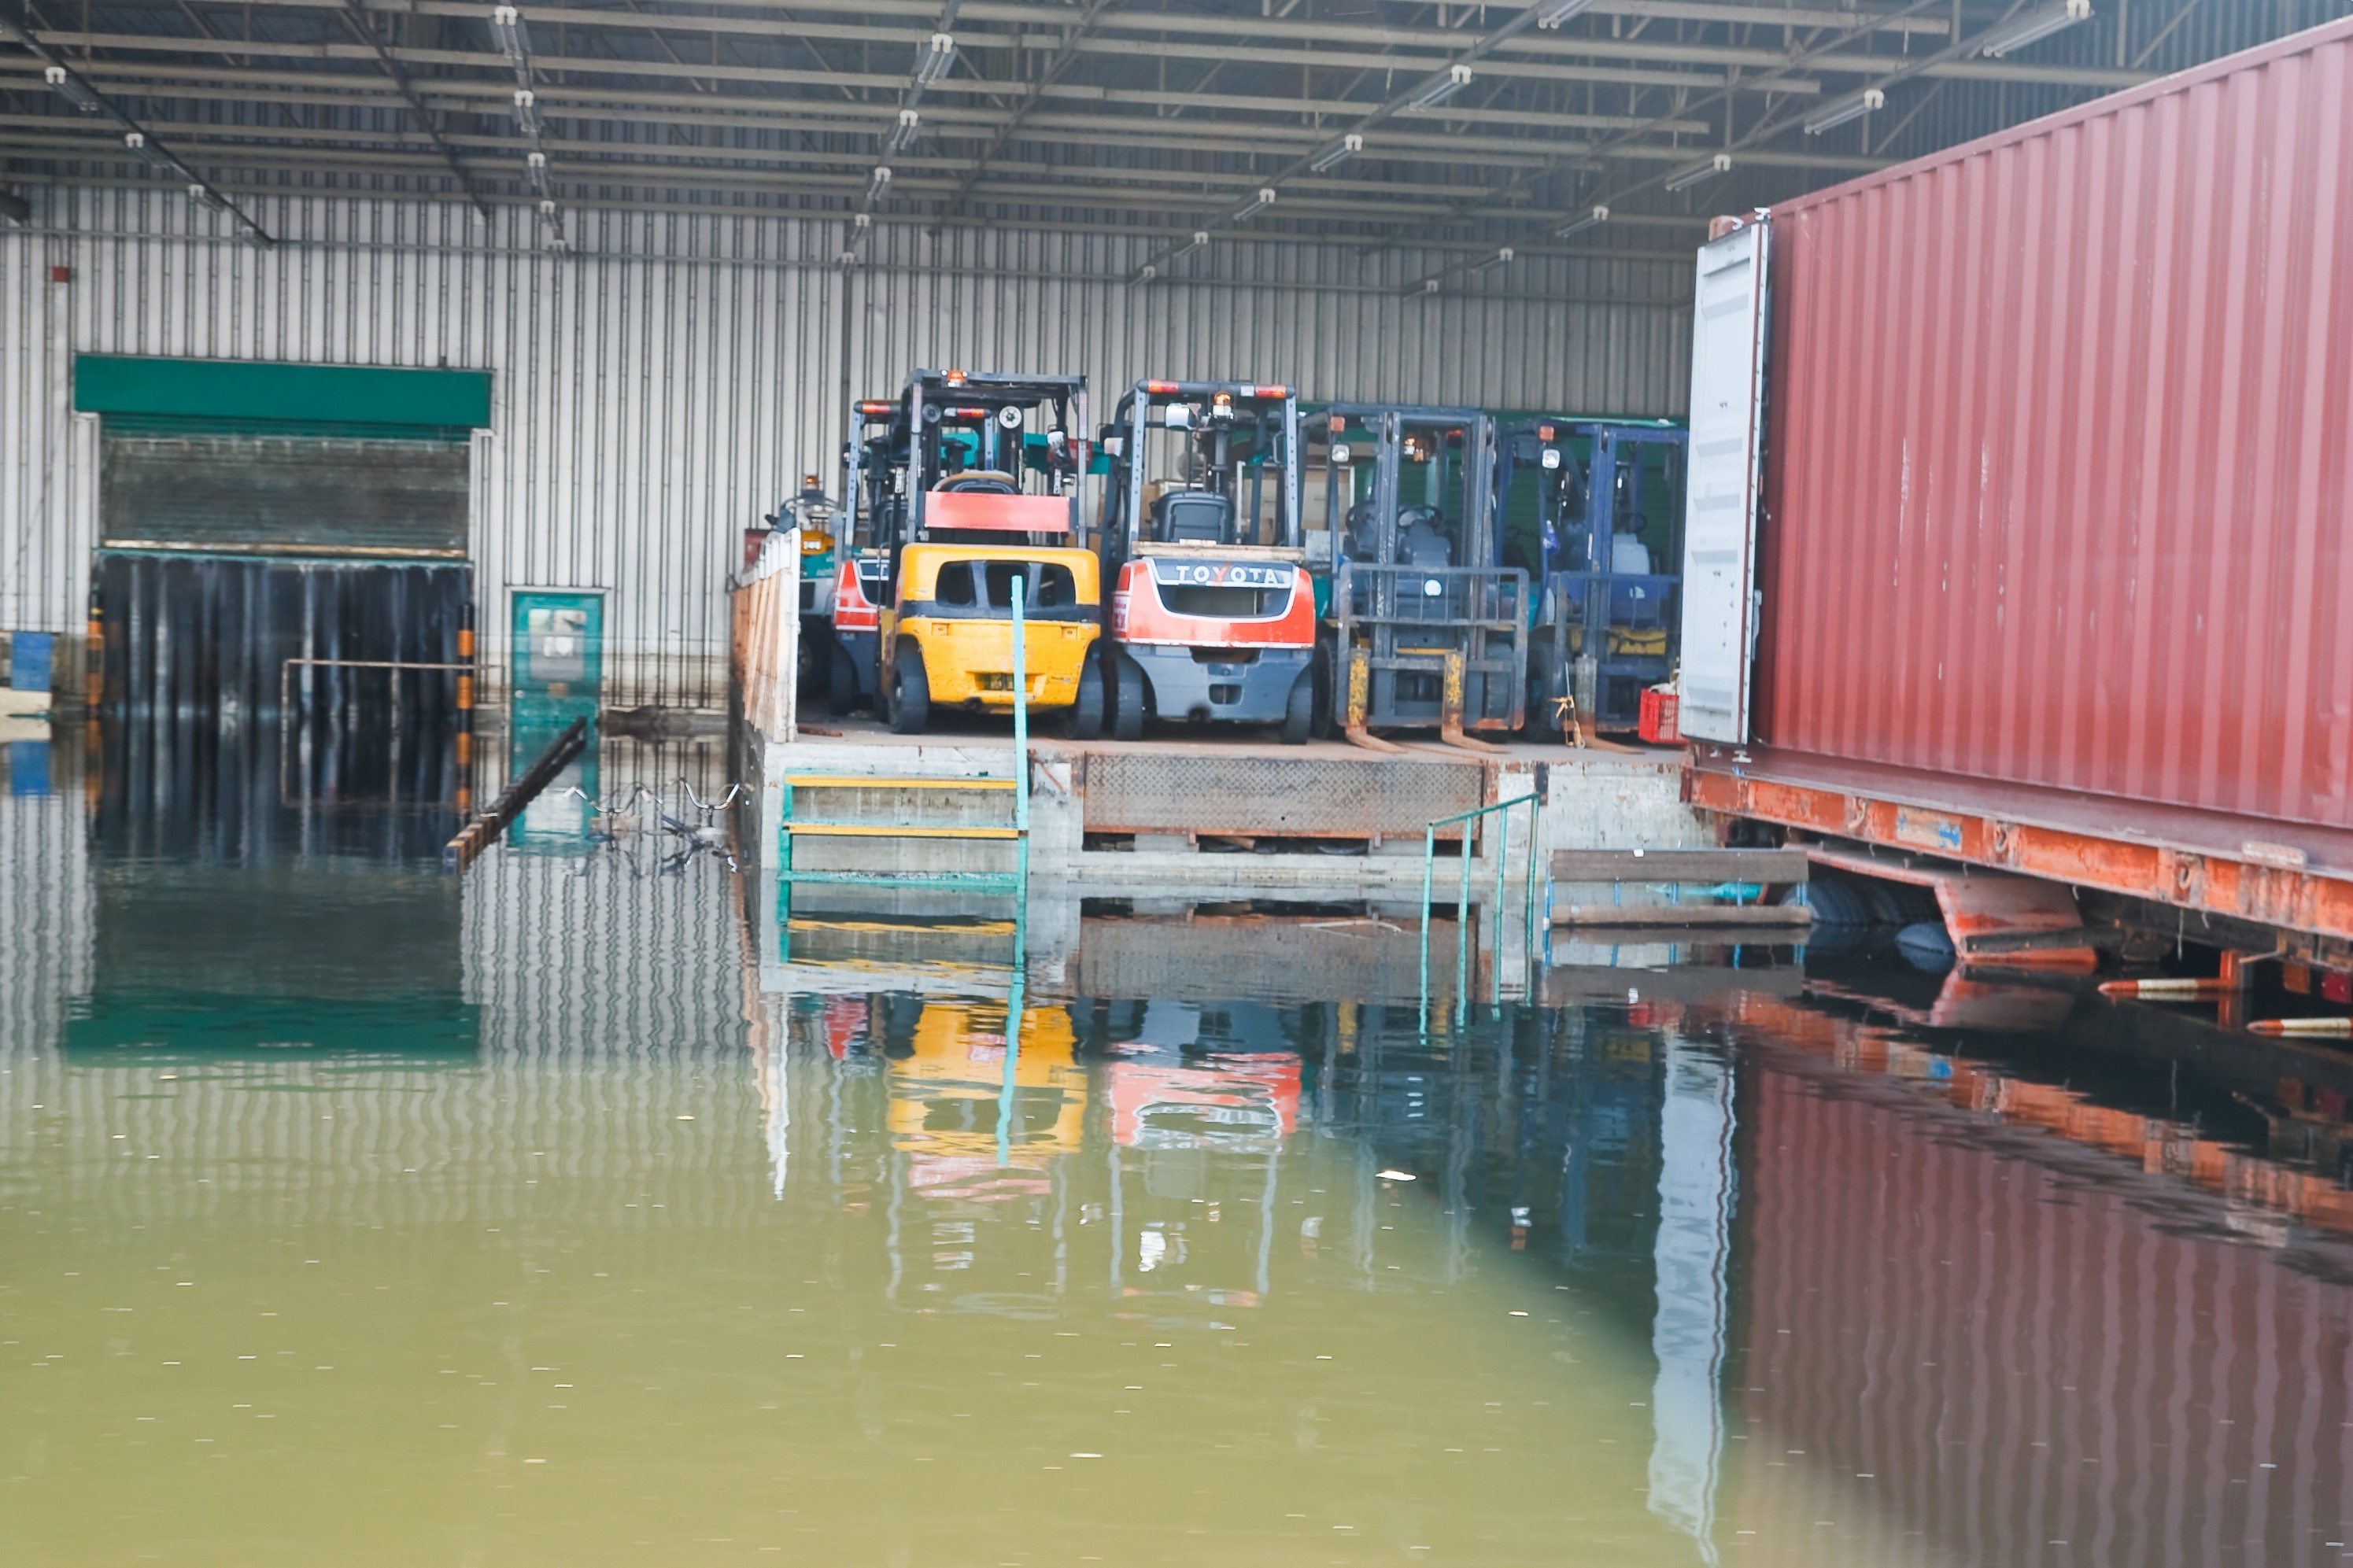
Do more to protect against floods – there is ‘Noah alternative’

Manufacturers should urgently review the condition of their drainage systems to guard against the risk of flooding, advises Kevin Moon, Managing Director of drainage and wastewater specialist Lanes Group plc.

The summer heatwave and subsequent warnings about flash floods demonstrates there is no room for complacency when it comes to factory site drainage as climate change takes hold.

Kevin Moon added: “We recommend that manufacturers review their flooding risks and the condition of their site drainage systems, as a key part of business continuity planning, as we head into autumn.

“Climate change is likely to put greater strain on site drainage systems. If they fail, the commercial consequences could be catastrophic.

“Making sure site drainage is in as good condition as possible, in terms of being free of debris that can disrupt water flows and reduce capacity and in good repair, should be a priority in situations like this.”

Lanes Group is the UK’s largest drainage and wastewater specialist. It helps thousands of businesses across the UK protect their properties through planned and reactive site drainage cleaning and maintenance services.

The company also delivers sewer unblocking, repair and rehabilitation services for many water companies, including Thames Water, Severn Trent, Northumbrian Water and Scottish Water.

Lanes has put together a 7-step check list to support a site drainage resilience review:

  1. Is your property location at particular risk of localised flooding?
  2. Do you have an accurate and up to date map of your site drainage system and assessments of its condition and capacity? These can only be obtained by a drainage specialist carrying out a full site CCTV drainage survey.
  3. Is the planned preventative maintenance schedule for the property’s drainage system up to date? Has the drainage system been cleaned in the last 12 months?
  4. Are you already experiencing any problems with your drainage system? Does water pool on surfaces around your property after it rains? Do sinks drain and toilets flush properly?
  5. Are water courses around your property in optimum condition? Are storm culverts serving your site regularly inspected and cleaned?
  6. Has there been any extensive building carried out recently that might affect your site drainage system?
  7. Do you have emergency preparations in place if a flood occurs? This may include access to an emergency response service from a reputable drainage specialist and plans to protect assets and deliver services from a different location.

Just like clean water pipes, surface water drains and sewers can be affected by the seasonal contraction and expansion of clay soils, resulting in pipe joints being displaced, pipes cracking or even collapsing.

This problem is expected to become more commonplace due to climate change, with northern areas of the UK increasingly affected for the first time due to changing weather patterns.

During prolonged periods of dry weather, tree root systems grow more aggressively as they search for water and nutrients, increasing the risk of root infestation of drainage pipes.

Low flow rates in sewers and surface water drains during dry weather allow heavier solid material and debris washed into the system to build up, compromising its capacity, increasing the risk of flooding.

Kevin Moon said: “Climate change is creating more volatile, more unpredictable weather. This, in turn, means the condition of site drainage systems can change more rapidly than in previous times.

“The only answer is to tighten planned preventative maintenance systems, with more frequent and thorough inspection and drain cleaning regimes, beginning with asking the questions detailed in our drainage resilience checklist.

“The alternative may be to expose business sites to greater risk of serious flooding events and the far greater costs they incur.”

www.lanesfordrains.co.uk

This website is owned and operated by: MSL Media Limited

msl logo
www.mslmedialtd.com

Co. Number: 05359182

© 2005 MSL Media Ltd. All rights reserved. E&OE

ems logo mobile